Titanium Anode vs Other Anodes: Core Electrochemical Comparison
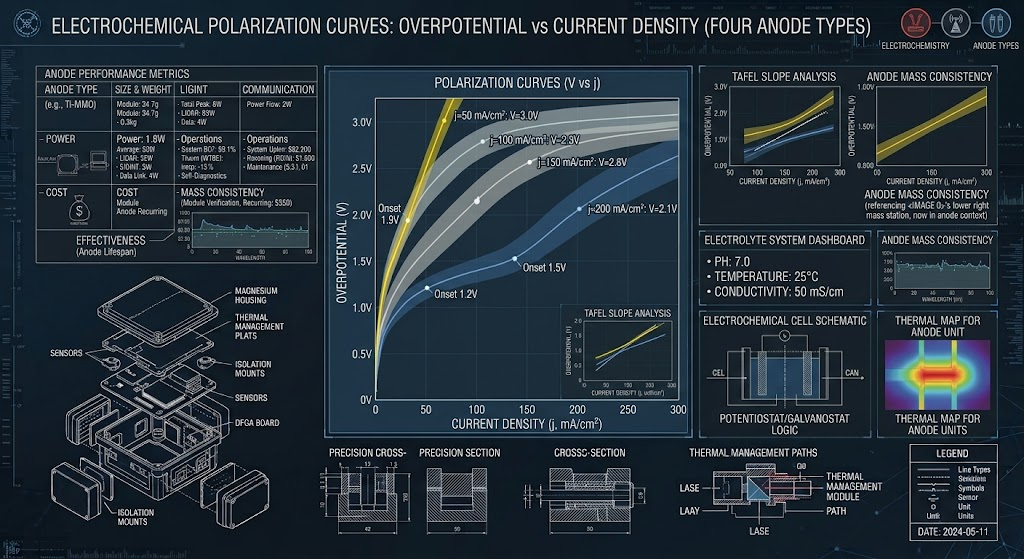
Modern electrochemical processes demand high electrocatalytic efficiency, absolute dimensional stability, and prolonged operational life. Dimensionally Stable Anodes (DSA) built on an ASTM B265 titanium plate substrate with Mixed Metal Oxide (MMO) electrocatalytic coatings replace consumable electrodes like graphite, lead alloys, and cast iron. They decrease total cell potential by 300 to 500 mV and completely eliminate toxic anode sludge.
Consumable anodes continuously lose mass during operation. This degradation alters the inter-electrode gap, skews electrical field uniformity, and drives up specific power usage (kWh/MT). MMO titanium anodes maintain steady geometric profiles down to ±0.2 mm over multi-year duty cycles.
Technical Evaluation Matrix: The Four Performance Pillars
Industrial electrochemical facility design balances upfront capital costs against operational efficiency. To establish a standardized benchmark, plant operators rely on our proprietary Electrochemical Cell Efficiency and Substrate Circularity (ECESC) Framework to evaluate anode longevity and system stability.
| Evaluation Dimension | MMO Coated Titanium (DSA) | Lead-Silver Alloy (Pb-0.5%Ag) | Synthetic Industrial Graphite | High-Silicon Cast Iron (HSCI) |
|---|---|---|---|---|
| 1. Overpotential & Cell Voltage | Low: ηOER ~300-380 mV, ηCER ~30-50 mV | High: ηOER ~750-900 mV | Very High: Polarization rises with erosion | Very High: ηOER >950 mV |
| 2. Dimensional Geometry | Invariant; maintains inter-electrode spacing ±0.2 mm | Variable; creeps, sags, and warps under heat | Degrades quickly; continuously spalls carbon | Sacrificial; structural dimensions erode |
| 3. Product Purity & Residue | Zero contamination; no metallic dissolution | Generates hazardous PbSO4 and PbO2 sludge | Heavy carbon particulate contamination | Heavy iron and silicon oxide residue |
| 4. Circularity & Refurbishment | Strip and recoat substrate 3-5 times | Melt and recast only (high energy loss) | Non-recyclable; solid waste disposal | Non-recyclable consumable; discarded |
Head-to-Head Material Benchmarks: Titanium vs Industrial Alternatives
Each anode technology relies on distinct electrochemical reaction dynamics. Selecting the wrong substrate material leads to elevated overpotential losses, higher maintenance overhead, and unwanted contamination in downstream products.
Titanium Anode vs Graphite: Mechanical Integrity and Current Density
Industrial graphite has long served as a baseline conductor in early chlor-alkali and electrodialysis cells. However, graphite anodes face physical disintegration caused by carbon matrix oxidation:
C + 2H2O → CO2 + 4H+ + 4e- (E° = 0.207 V vs. SHE)
Simultaneous carbon oxidation and mechanical erosion degrade graphite rapidly. This limits practical operating current densities below 800 A/m2.
Carbon particles slough into the electrolyte, clogging ion-exchange membranes and requiring frequent filtration runs. Upgrading cells to MMO-coated corrosion-resistant Grade 1 titanium allows continuous operation above 10,000 A/m2 without particulate generation, cutting down-cell maintenance windows to zero.
Titanium Anode vs Lead-Silver (Pb-Ag): Energy Consumption & Sludge Elimination
In base metal electrowinning (copper, zinc, and cobalt), rolled or cast lead-silver (Pb-0.5% to 1.0% Ag) alloys have served as traditional workhorses. Despite low initial procurement costs, Pb-Ag anodes impose significant thermodynamic and operational penalties.
Pb-Ag exhibits an oxygen evolution reaction (OER) overpotential roughly 400 mV higher than specialized IrO2-Ta2O5 coated titanium. Applying the Nernst-derived power equation reveals the scale of this penalty:
Psaved (kWh/MT) = (ΔVcell × n × F) / (3600 × M × εc)
A cell voltage reduction of ΔVcell = 0.40 V yields roughly 340 to 420 kWh of direct DC energy savings per metric ton of cathode metal extracted (assuming 92% cathode current efficiency, εc).
Pb-Ag anodes also shed hazardous lead sulfate (PbSO4) and lead dioxide (PbO2) sludge. This debris settles in electrowinning cells, creates short-circuit dendrites, and co-deposits onto the cathode, lowering commercial metal purity grades. Titanium DSA systems remove lead waste streams entirely, yielding purer products while supporting modern environmental compliance programs.
Titanium Anode vs Solid Platinum & Platinized Substrates: Capex and TCO
Solid platinum sheets deliver exceptional catalytic kinetics, but their capital expense makes full-scale industrial use impractical. Platinized titanium (electroplated metallic Pt on titanium) offers a partial compromise, yet it remains prone to rapid dissolution in acidic, chloride-bearing electrolytes.
Platinum electroplates dissolve at approximately 1 to 3 μg/A·h under reverse-pulse conditions or elevated temperatures. Conversely, thermally sintered IrO2-Ta2O5 and RuO2 mixed metal oxides create solid-solution, rutile-phase crystalline films. These deliver equal catalytic activity while keeping initial coating expenses 70% to 85% below solid precious metal sheets.
Titanium Anode vs High Silicon Cast Iron (HSCI): Cathodic Protection Durability
In Impressed Current Cathodic Protection (ICCP) systems protecting pipelines, marine infrastructure, and storage tanks, High Silicon Cast Iron (HSCI) anodes require heavy material volumes to offset high consumption rates (0.1 to 0.5 kg/A·year). Their brittle nature leads to cracking during offshore installation and deep-well drilling.
Solid titanium ribbon and tubular strings coated with mixed metal oxides weigh just 5% to 10% of equivalent HSCI arrays. Operating with consumption rates under 2 to 5 mg/A·year per standard NACE TM0108 protocols, MMO titanium minimizes drill-hole footprints, speeds up installations, and cuts groundbed resistance over decades of continuous protection.
Electrochemical Thermodynamics: CER vs OER Reaction Kinetics
Electrochemical efficiency depends on matching the catalyst structure to the target electrolytic reaction. MMO catalysts are formulated to split along two distinct electrochemical reaction paths:
The Chlorine Evolution Reaction (CER) operates via a two-electron transfer mechanism (2Cl- → Cl2 + 2e-). Industrial chlor-alkali and ballast water systems utilize RuO2-TiO2 and RuO2-IrO2 coatings to lower the chlorine overpotential below 50 mV at 3,000 A/m2, keeping parasitic oxygen evolution under 1.5%.
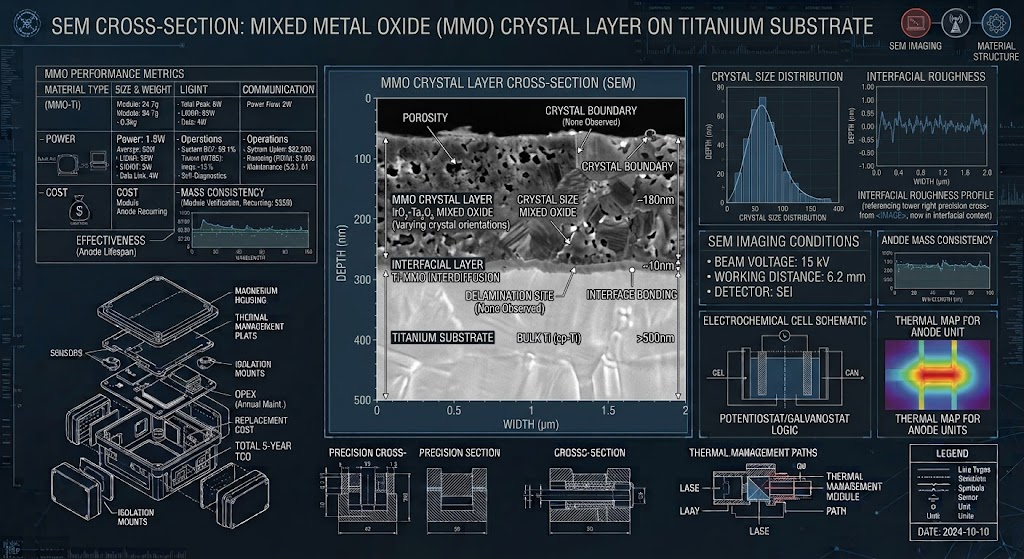
For the Oxygen Evolution Reaction (OER) in sulfuric, nitric, and methanesulfonic acid electrolytes (2H2O → O2 + 4H+ + 4e-), ruthenium degrades through high-valence volatility (forming gaseous RuO4). In these environments, IrO2-Ta2O5 mixed-oxide solutions stabilize the crystal structure, yielding low Tafel slopes (35 to 45 mV/dec) that resist aggressive acid attack.
Extreme Operating Environments: Engineering Solutions for Hostile Cells
Standard industrial anodes break down rapidly in non-standard chemistries. At China Titanium Factory, our metallurgists customize base formulations to handle high-stress operating edge cases.
High-Fluoride Acidic Electrolytes: Fluoride ions (F-) penetrate oxide barriers and dissolve titanium base metal via fluotitanate reactions [Ti + 6HF → H2TiF6 + 2H2]. We apply an intermediate, highly dense Ta2O5-SnO2 sealing layer beneath the active catalyst, preventing electrolyte penetration even at dissolved fluoride levels above 30 mg/L.
Anti-Scaling Polarity Reversal Systems: Water treatment and electro-chlorination cells reverse polarity to shed cathode scale, triggering rapid catalyst stripping on typical anodes. We engineer balanced IrO2-RuO2-Pt structures with matching surface work functions, sustaining over 20,000 automated reversal cycles without catalyst delamination.
Ultra-High Current Density PCB Foil Plating: Operating copper foil deposition systems above 100 A/dm2 generates heavy gas bubble erosion. Deploying precision titanium mesh anodes cut from expanded Grade 1 sheet optimizes fluid dynamics, sheds micro-bubbles quickly, and prevents localized overpotential hot-spots.
High-Current Busbar Transitions: Electrowinning plants require robust mechanical joints between copper power supplies and titanium cell hardware. We provide custom CNC titanium machining to fabricate explosion-bonded copper-clad titanium busbars, keeping contact resistance below 15 μΩ.
The China Titanium Quality Protocol: Substrate Metallurgy & Sintering Standards
Electrode operational life depends heavily on metallurgical adhesion at the substrate boundary. China Titanium Factory implements an uncompromising production framework:
ASTM B265 Grade 1 Chemistry: We use ultra-low interstitial titanium (Fe ≤ 0.20%, C ≤ 0.08%, N ≤ 0.03%, H ≤ 0.015%, O ≤ 0.18%) to prevent micro-embrittlement along weld seams.
Mechanical Substrate Profiling: We blast parts with high-purity corundum grit to achieve a uniform surface roughness (Ra 2.5 to 3.5 μm), maximizing surface area for catalytic bonding.
Chemical Hydride Etching: Components undergo chemical etching in boiling 20% hydrochloric acid to dissolve native air-formed TiO2 barriers and build a micro-rough titanium hydride (TiH2) base.
Precision Sol-Gel Application: Automated pneumatic systems apply analytical-grade ruthenium, iridium, tantalum, and platinum chloride salts evenly across the substrate.
Multi-Stage Thermal Calcination: Stepwise sintering in computerized industrial kilns (380°C to 500°C) oxidizes metallic salts into catalytic rutile solid solutions while avoiding substrate thermal distortion.
Engineering Insight: We verify precious metal loading on every production lot using X-ray fluorescence (XRF) per ISO 3497 standards. Coating adhesion must meet ASTM D3359 Method B cross-cut tape inspection requirements (achieving a 4B/5B rating) before material release.
Lifecycle Economics and Recoating Engineering: Saving 60% on Replacement OPEX
Unlike consumable lead or carbon electrodes that are discarded after use, titanium is a permanent capital asset. When catalytic coatings reach the end of their operational service life, the underlying titanium plate, mesh, or tube remains structurally sound.
Through our dedicated electrode refurbishment program, spent anodes undergo non-destructive chemical stripping to eliminate depleted oxides without pitting the parent metal. Following surface re-profiling and secondary chemical etching, fresh catalyst coatings are applied and sintered.
Refurbishing and recoating anodes reduces capital expenses by 50% to 60% compared to purchasing new assemblies. This reuse cycle lowers overall plant operating costs and prevents high-purity structural metal from entering the waste stream.
Frequently Asked Questions: Industrial Procurement & Performance Validation
In copper electrowinning, how does MMO Titanium TCO compare to Lead-Silver over 5 years?
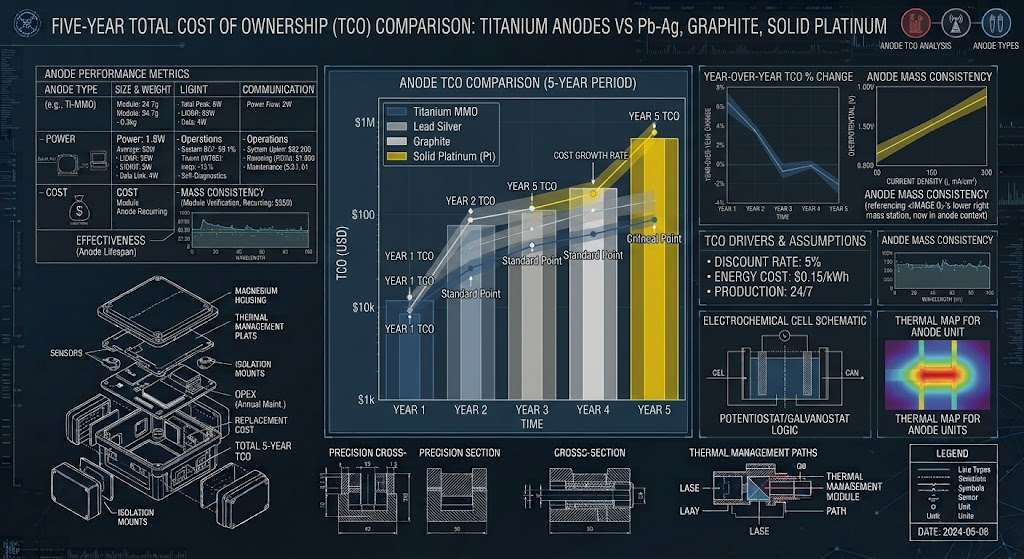
While Pb-Ag anodes cost roughly 30% less up front, MMO titanium delivers a 35% to 48% reduction in total ownership cost within 24 months. Operating at a 300 to 450 mV lower cell voltage cuts electricity consumption by roughly 300 to 420 kWh per ton of cathode output. MMO systems also avoid lead hazard compliance fees, save on cell maintenance, and retain the original titanium substrate for low-cost recoating.
How can an engineer verify precious metal loading and coating adhesion before deployment?
Plant quality teams verify materials through three independent tests: First, review the supplier EN 10204 3.1 Mill Test Certificate with accompanying XRF thickness scans to ensure proper precious metal loads (typically ≥12 g/m2 for OER and ≥8 g/m2 for CER). Second, require Accelerated Life Testing data matching NACE TM0108 protocols (10,000 A/m2 in 1.0 M H2SO4 lasting over 150 hours). Third, run ASTM D3359 cross-hatch adhesion evaluations to confirm the coating resists flaking.
What is the typical manufacturing lead time for custom DSA designs?
Standard flat plate, mesh, and rod profiles ship within 7 to 10 working days. Complex assemblies requiring custom busbar machining, structural roll-forming, or custom robotic welding take 2 to 3 weeks for full manufacturing, XRF validation, and global logistics dispatch.
How to Order Custom MMO Titanium Anodes: 3-Step Production Pathway
Upgrading electrochemical plant infrastructure requires precise engineering collaboration. China Titanium Factory uses a structured three-step process to transition cells from CAD models to active plant deployment:
Submit Specifications & CAD Models: Upload drawing packages (.dwg, .step, or .pdf) along with key system parameters: working electrolyte chemistry, design pH, operational temperature, target current density (A/m2), and required operational lifespan.
Engineering Review & Optimization: Our metallurgists evaluate your cell configuration within 24 hours. We verify mechanical tolerances, select the ideal ASTM titanium substrate, and formulate the exact noble metal ratio (RuO2, IrO2, Ta2O5, SnO2, Pt) to match your operating bath.
Precision Sintering & Certified Logistics: Following production, every lot receives non-destructive XRF coating verification, tape adhesion validation, and full EN 10204 3.1 inspection certification before export packaging and worldwide transit.