Engineering Evaluation Matrix: The Four Pillars of Titanium Piping Superiority
Industrial titanium piping provides complete immunity to chloride-induced pitting, stress corrosion cracking (SCC), and severe oxidizing acids by continuously regenerating a tenacious titanium dioxide (TiO2) surface film. With a density of 4.51 g/cm3 and tensile strength up to 895 MPa, titanium pipes allow structural wall thinning down to Schedule 10S while delivering an operating life exceeding 25 years without corrosion allowance allowances.
Process plant reliability depends on four fundamental engineering criteria: operational fluid chemistry, structural payload limits, thermodynamic transfer efficiency, and long-term asset capitalization. Selecting materials for industrial piping often forces plant engineers to weigh initial capital expenditure against catastrophic failure risks.
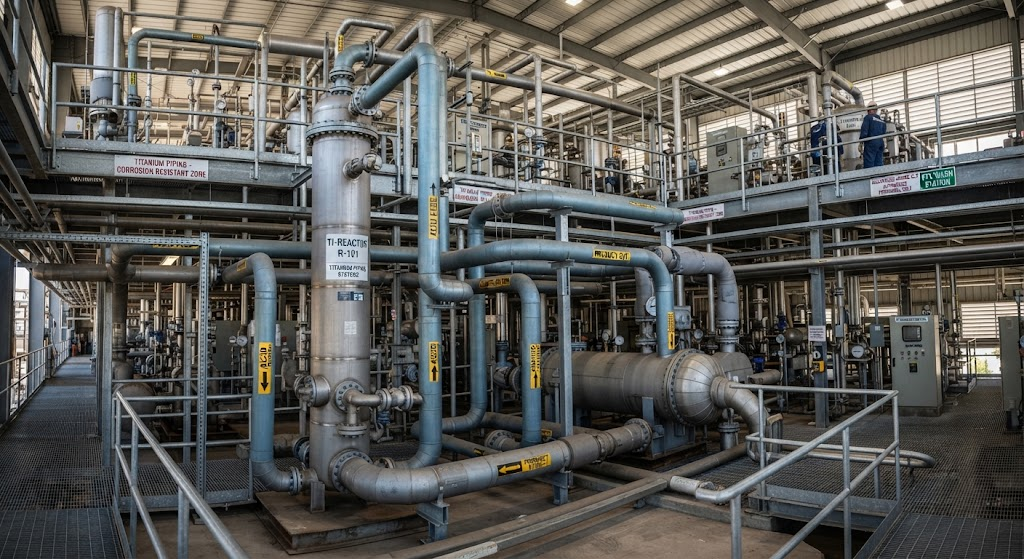
To establish a rigorous design standard, industrial plant systems evaluate piping materials through four definitive metrics:
Corrosion Resistance Margin (CRM): Titanium exhibits an electrochemical corrosion rate below 0.001 mm/year in aerated seawater, wet chlorine gas, and nitric acid streams across temperature ranges up to 250°C.
Wall Thickness Optimization (WTO): Because titanium resists uniform and localized wall loss, designers specify thin-wall schedules (Schedule 5S and Schedule 10S) rather than the heavy Schedule 40S/80S configurations mandatory for carbon and standard stainless steels.
Zero-Corrosion-Allowance Design (ZCA): The elimination of the standard 2.0 mm to 4.0 mm structural corrosion buffer maximizes inner pipe diameter, reduces pressure drop, and lowers dynamic pumping energy consumption.
20-Year Lifecycle Capitalization: While initial material costs exceed standard grades, zero maintenance shutdowns and extended operational uptime reduce total lifecycle costs by 30% to 55% compared to high-nickel alloys and super duplex steels.
Core Metallurgical Advantages: Oxide Passivation & Mechanical Integrity
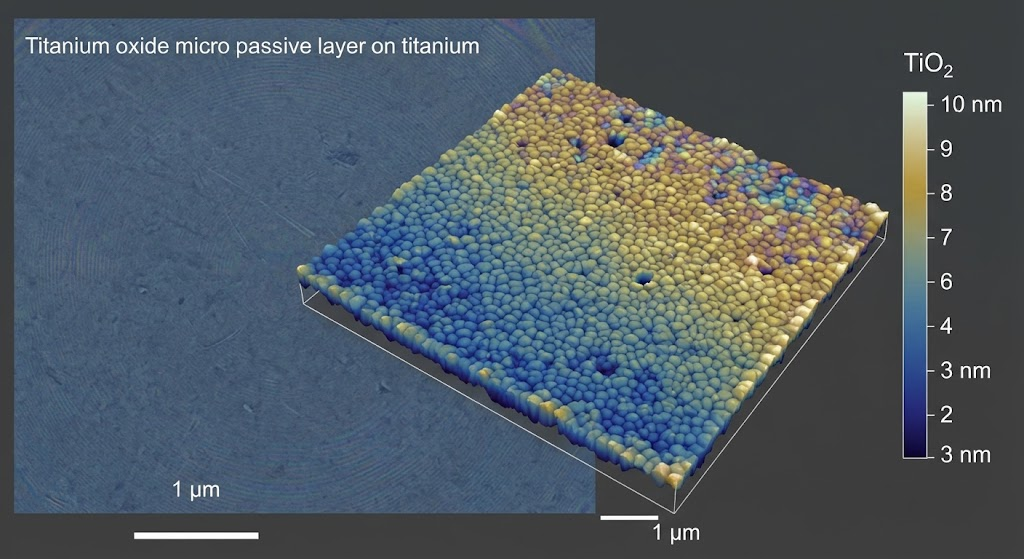
The operational endurance of industrial titanium pipe stems from solid-state surface thermodynamics. When exposed to even trace amounts of oxygen or moisture (down to parts-per-million concentrations), raw titanium instantaneously forms a dense, continuous film of rutile and anatase titanium dioxide (TiO2).
This ceramic-like oxide film ranges from 10 nm to 20 nm in thickness. If mechanical damage, particulate scouring, or hydraulic impact breaches the surface, the film self-repairs instantaneously in ambient and chemical fluid streams.
For standard piping runs carrying corrosive industrial effluents, cooling water, and brine, Grade 2 commercially pure titanium provides the optimal balance of mechanical ductility, moderate yield strength, and broad chemical passivity.
| Material Grade | Density (g/cm3) | Yield Strength (MPa) | Tensile Strength (MPa) | Elastic Modulus (GPa) | Thermal Cond. (W/m·K) |
|---|---|---|---|---|---|
| Titanium Gr 2 (UNS R50400) | 4.51 | 275 - 410 | ≥ 345 | 105 | 21.9 |
| Titanium Gr 5 (Ti-6Al-4V) | 4.43 | ≥ 828 | ≥ 895 | 114 | 6.7 |
| Super Duplex 2507 (UNS S32750) | 7.80 | ≥ 550 | 750 - 1000 | 200 | 15.0 |
| 316L Stainless (UNS S31603) | 8.00 | ≥ 220 | 520 - 680 | 193 | 16.3 |
In cryogenic environments, titanium alloys maintain high impact toughness without showing a ductile-to-brittle transition temperature (DBTT). Titanium pipes operate reliably down to -196°C in liquid nitrogen and liquefied natural gas (LNG) systems, whereas ferritic and duplex alloys suffer severe low-temperature embrittlement.
Tailored Alloy Selection for Severe Industrial Operating Environments
Standard process lines do not encounter uniform chemical threats. Selecting the appropriate titanium alloy grade ensures the piping system withstands extreme chemical media, aggressive flow regimes, and high thermal profiles.
High-Pressure and Severe Chemical Lines
For high-pressure reactors, severe oxidizing environments, and critical chemical loops, engineers specify ASTM B861 seamless titanium pipe. Cold-drawn and vacuum-annealed seamless pipes remove weld-seam discontinuity risks under cyclic pressure loads.
Reducing Acid Media (HCl, H2SO4): Grade 7 (Ti-0.15Pd) and Grade 11 contain palladium additions that shift the mixed corrosion potential into the passive zone. This stops localized attack in non-aerated acidic solutions up to boiling temperatures.
Crevice-Prone Brine Services: Grade 12 (Ti-0.3Mo-0.8Ni) provides cost-effective crevice and pitting resistance in high-temperature hypersaline solutions (pH 3 to 11 at temperatures above 100°C), preventing localized breakdown under flange gaskets.
Large-Diameter Seawater and Effluent Infrastructure
For power generation intake systems, desalination intake mains, and chlor-alkali header lines, plant engineers select welded titanium pipes ASTM B862. Automatic plasma arc and TIG welding processes deliver consistent weld root penetration and clean metallurgical grain boundaries across nominal diameters up to DN1200 (48 inches).
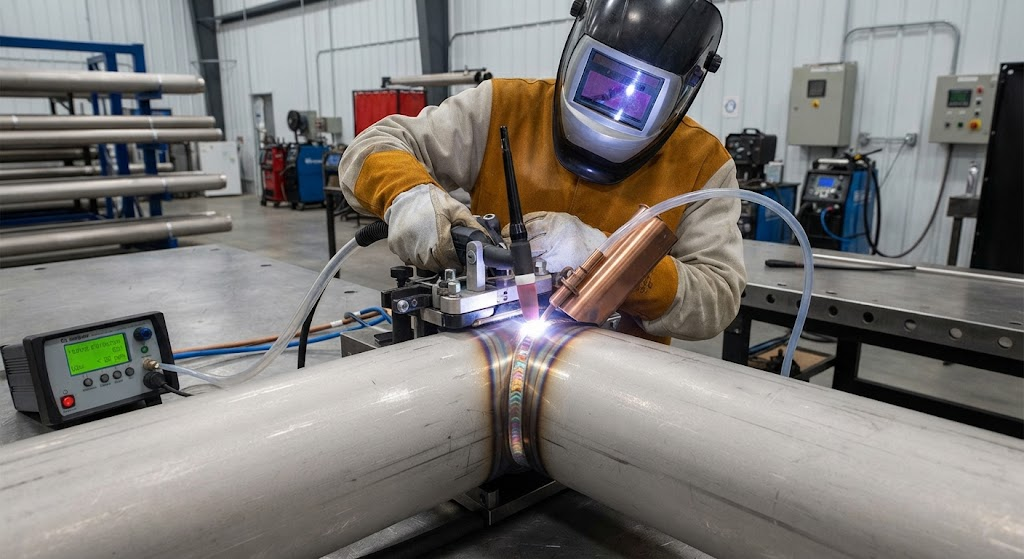
According to technical guidelines published by ASTM International and materials degradation standards from AMPP (Association for Materials Protection and Performance), titanium maintains zero pitting rate (PREN equivalent > 45) in ambient and hot marine environments.
20-Year Total Cost of Ownership (TCO): Titanium Gr 2 vs Super Duplex 2507 vs 316L SS
Procurement teams often compare initial pipe procurement prices directly per kilogram. However, this metric overlooks structural density, schedule reductions, and plant downtime expenses.
Because titanium's density is approximately 56% that of stainless steel, a linear meter of titanium pipe at equivalent wall thickness weighs almost half as much as steel. Combined with zero corrosion allowance (allowing Schedule 10S instead of Schedule 40S), raw material weight drops by 60% to 70% per meter run.
| Cost Parameter | Titanium Gr 2 (Sch 10S) | Super Duplex 2507 (Sch 40S) | 316L Stainless (Sch 40S) |
|---|---|---|---|
| Initial Material Cost Index | 1.35× | 1.20× | 1.00× (Baseline) |
| Structural Piping Mass (kg) | 3,850 kg | 12,900 kg | 13,200 kg |
| Structural Support Capex | Low (-45%) | High (Baseline) | High (Baseline) |
| Expected Service Lifespan | > 25 Years | 8 - 12 Years | 3 - 5 Years |
| 20-Year Replacements Required | 0 | 1 - 2 | 3 - 4 |
| Total 20-Year TCO Index | 1.00× (Lowest) | 1.85× | 2.90× |
Completing piping runs requires matching elbows, tees, reducers, and stub ends. Using fully compatible custom titanium pipe fittings and flanges built to ASME B16.9 and ASME B16.5 standards preserves system-wide metallurgical continuity and prevents galvanic couples.
Manufacturing Standards & QA/QC Integrity: The China Titanium Quality Protocol
Piping reliability depends on strict quality controls during melting, extrusion, and welding. Impurities like excess interstitial hydrogen, carbon, or oxygen cause embrittlement and micro-fissuring during thermal cycling.
China Titanium Factory enforces a dedicated 5-stage manufacturing and verification procedure to maintain complete alloy integrity:
Vacuum Arc Remelting (VAR) Control: Ingots undergo double or triple VAR melting to ensure clean ingot chemistry, tight grain structures, and compliance with ASTM interstitial limits (O ≤ 0.25%, N ≤ 0.03%, H ≤ 0.015% for Grade 2).
Precision Tube Rolling and Sizing: Cold pilgering and multi-pass drawing maintain uniform wall thickness (tolerances within ±5%) and surface roughness (Ra ≤ 0.8 μm).
100% Non-Destructive Testing (NDT): Every pipe length undergoes full ultrasonic testing (ASTM E213) or eddy current inspection (ASTM E426) to detect subsurface inclusions and longitudinal flaws.
Hydrostatic & Pneumatic Proof Testing: Full-pressure hydraulic validation according to ASME Section VIII / B31.3 ensures hoop-stress integrity without plastic deformation or joint leakage.
EN 10204 3.1 Traceability: Complete Mill Test Certificates (MTC) deliver lot-by-lot tracking of chemical composition, tensile yield curves, flattening tests, and flaring verifications.
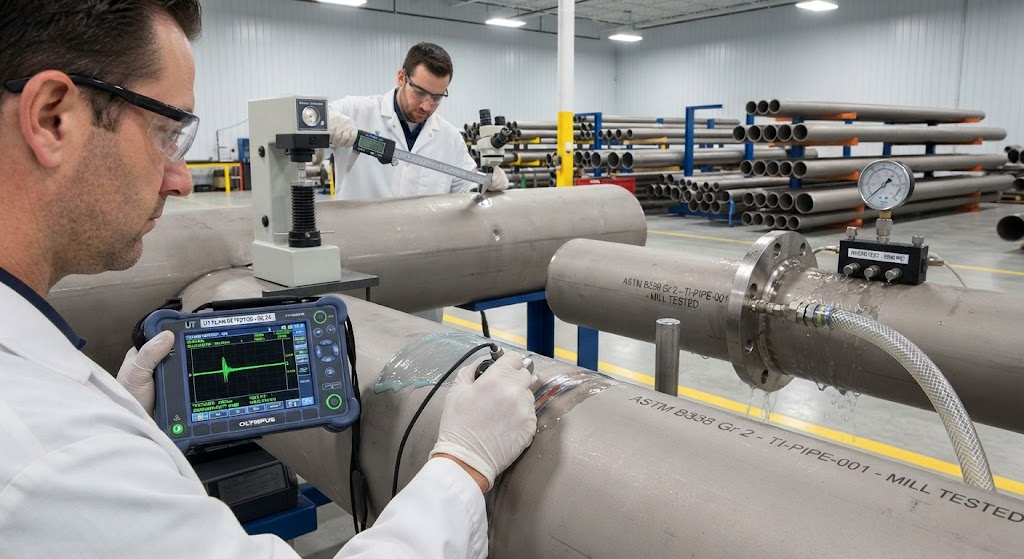
All piping lots comply with international standards, including ASTM B861 (seamless), ASTM B862 (welded), ASTM B338 (condenser tubes), DIN 17861, and European Pressure Equipment Directive (PED 2014/68/EU).
Authenticity Verification & Procurement Truths: Critical Engineering FAQ
Is Titanium Pipe more cost-effective than Duplex 2205 or Super Austenitic Stainless Steel?
Yes. While titanium carries a higher initial raw material cost per kilogram, its low density (4.51 g/cm3 vs 7.80 g/cm3 for Duplex) and zero corrosion allowance design allow engineers to specify Schedule 10S rather than Schedule 40S. This cuts total pipe mass by up to 45%. In seawater cooling and chlor-alkali services where Duplex 2205 experiences pitting within 3 to 5 years, titanium operates for 25+ years without maintenance downtime, yielding a 30% to 55% lower 20-year Total Cost of Ownership.
How do plant engineers verify the authenticity and weld integrity of imported Titanium Pipes?
Piping shipments must be accompanied by an authentic EN 10204 Type 3.1 Inspection Certificate matching the heat numbers stamped directly on the pipe OD. In our manufacturing facilities, chemical verification involves handheld Positive Material Identification (PMI) and optical emission spectrometry. Weld seam integrity is confirmed through 100% Eddy Current testing, radiographic examination (RT), and mechanical flattening tests where the tube is compressed to a calculated height (H) without cracking along the weld line.
What is the maximum operating temperature limit for industrial titanium pipes?
Commercially pure titanium (Grades 1, 2, 3, 4) operates continuously in oxidizing atmospheres and process lines up to 315°C (600°F). Above 400°C, atmospheric oxygen and hydrogen diffuse into the metal lattice, causing interstitial embrittlement. For higher temperature ranges and elevated structural pressures, Grade 5 (Ti-6Al-4V) or specialized near-alpha titanium alloys should be selected.
Initiating Your Titanium Piping Project: Direct Engineering Pathway
Transitioning process infrastructure from legacy steel alloys to high-efficiency titanium piping is straightforward through our direct mill workflow:
Step 1: Upload Requirements
Submit process media parameters (temperature, pressure, fluid chemistry, flow velocity) and isometric piping drawings.
Step 2: DFM & Schedule Review
Our metallurgists perform a design-for-manufacturing review, optimizing wall schedules and generating competitive mill-direct quotations.
Step 3: Certified Dispatch
Receive fully tested ASTM/ASME certified titanium pipes with complete EN 10204 3.1 mill test certificates and third-party inspection.
Optimize Your Industrial Piping Infrastructure
Connect directly with China Titanium Factory's metallurgy team to review chemical tolerances, schedule savings, and project specifications.
Request an Engineering Quote