Selecting between Ruthenium-Iridium (RuO2-IrO2) and Iridium-Tantalum (IrO2-Ta2O5) dimensionally stable anodes (DSA) depends strictly on electrolyte chemistry, target reaction kinetics, and anodic polarization potentials. Ru-Ir formulations provide superior catalytic activity for halogen-generating oxidation, whereas Ir-Ta systems provide high electrochemical stability against lattice dissolution in aggressive oxygen-evolving acid matrices.
Both systems rely on a valve-metal base—typically an unalloyed Grade 1 titanium substrate—coated with mixed metal oxides (MMO) via thermal decomposition. The fundamental metallurgical divergence lies in the active electrocatalyst and its stabilizing oxide matrix:
Mixed Metal Oxide (MMO) Anode: An insoluble electrode comprising an electroconductive, corrosion-resistant valve metal substrate (primarily ASTM B265 titanium) activated with a crystalline, semi-conductive solid-solution oxide layer (such as RuO2, IrO2, Ta2O5, or TiO2) engineered to lower electrochemical overpotential for specific oxidation pathways.
The catalytic performance rests on the solid-solution formation between isomorphic rutile structures. RuO2 and IrO2 possess tetragonal rutile lattices, allowing complete miscibility. In Ir-Ta systems, amorphous Ta2O5 acts as a film-forming, non-conductive stabilizing matrix that isolates the IrO2 active sites, preventing rapid dissolution during intense Oxygen Evolution Reactions (OER).
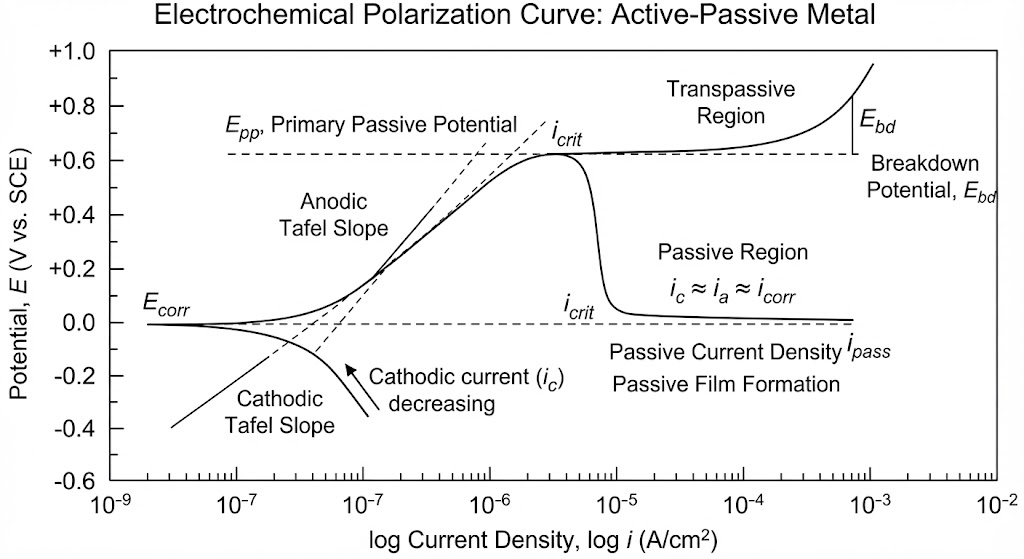
The thermodynamic and kinetic operational envelopes of Ru-Ir and Ir-Ta systems are governed by the competition between the Chlorine Evolution Reaction (CER) and the Oxygen Evolution Reaction (OER).
In aqueous sodium chloride environments, the primary anodic reaction is the oxidation of chloride ions to dissolved chlorine gas:
2Cl- → Cl2(g) + 2e- (E° = +1.358 V vs. SHE)
Ruthenium dioxide exhibits the lowest known overpotential for this pathway (η < 40 mV at 2,000 A/m²). Ru-Ir coatings operate via the catalytic Krishtalik mechanism, where chloride ions form an intermediate surface complex with active ruthenium sites (Ru4+/Ru3+ redox couple). This lowers the activation energy and prevents side-reaction oxygen evolution up to current densities exceeding 4,000 A/m².
In sulfate, nitrate, or phosphate media devoid of halides, the dominant pathway is the oxidation of water molecules:
2H2O → O2(g) + 4H+ + 4e- (E° = +1.229 V vs. SHE)
Although thermodynamically favored over CER, OER involves a complex four-electron transfer step exhibiting slow reaction kinetics. Under acidic conditions (pH < 1), standard RuO2 coatings undergo accelerated oxidation to volatile, soluble ruthenium tetroxide (RuO4), causing rapid coating deactivation within days. In contrast, IrO2-Ta2O5 catalysts suppress dissolution via strong iridium-tantalum d-electron orbital overlapping, maintaining stable OER overpotentials (η ≈ 280–350 mV at 5,000 A/m²) across thousands of operational hours.
Operating conditions determine the ideal coating chemistry. The performance metrics below represent standardized factory baselines evaluated per ASTM B265 and NACE TM0108 industrial parameters.
| Parameter | Ru-Ir Coated Titanium (RuO2-IrO2-TiO2) | Ir-Ta Coated Titanium (IrO2-Ta2O5) |
|---|---|---|
| Primary Target Reaction | Chlorine Evolution Reaction (CER) | Oxygen Evolution Reaction (OER) |
| Standard Noble Metal Ratio (Molar %) | Ru:Ir = 70:30 (or 65:15:20 Ru:Ir:Ti) | Ir:Ta = 65:35 to 70:30 |
| Noble Metal Loading Density | 8.0 – 15.0 g/m² (Application-tuned) | 12.0 – 25.0 g/m² (Electrowinning grades) |
| Coating Thickness Range | 2.0 – 5.0 μm (15–25 thermal coats) | 3.0 – 8.0 μm (20–35 thermal coats) |
| Evolution Overpotential | < 1.12 V vs. SCE (in 4M NaCl) | < 1.45 V vs. SCE (in 1M H2SO4) |
| Polarization Resistance | Low charge-transfer resistance (Rct ≤ 0.8 Ω·cm²) | Moderate-low charge-transfer resistance (Rct ≤ 1.5 Ω·cm²) |
| Allowable Electrolyte pH Range | pH 2.0 – 12.0 (Degrades at pH < 1.5) | pH 0.0 – 10.0 (High stability in pH < 1.0) |
| Standard Operating Current Density | 500 – 3,500 A/m² | 1,000 – 12,000 A/m² (High-speed lines) |
| Accelerated Life (HG/T 2471-2017) | > 80 hours (1.0 M H2SO4 @ 20,000 A/m²) | > 250 hours (1.0 M H2SO4 @ 20,000 A/m²) |
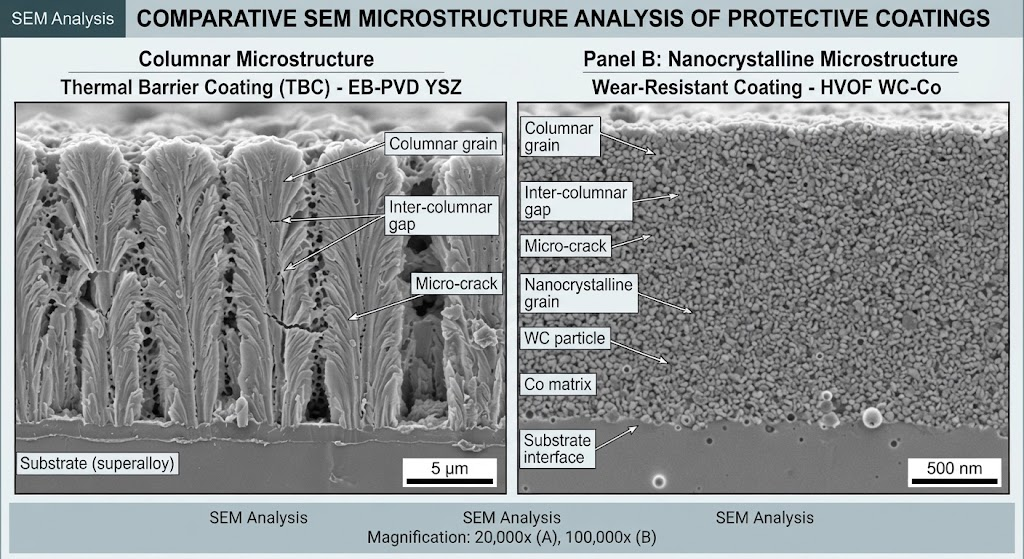
MMO anode failure typically stems from mechanical delamination or interfacial oxidation rather than catalytic consumption. China Titanium Factory addresses this through the Dual-Phase Thermo-Catalytic (DTC) Protocol, a 7-stage manufacturing process designed to maximize coating-to-substrate adhesion.
Chemical Degreasing & Mechanical Blasting: Substrates are processed using angular Al2O3 media to establish a continuous surface roughness of Ra = 3.5–5.0 μm.
Oxalic Acid Hydride Etching: Boiling in 10% wt oxalic acid at 95°C generates a uniform titanium hydride (TiH2) micro-pitted anchor morphology.
Intermediate Barrier Layer Application: Thermal deposition of a dense TiO2-Ta2O5 conductive sublayer blocks atomic oxygen diffusion into the base metal.
Precursor Salt Formulation: Liquid-phase ultrasonic blending of ionic ruthenium and iridium chlorides or tantalum alkoxides in anhydrous alcohol carriers.
Layer-by-Layer Robotic Micro-Coating: Computer-controlled pneumatic atomization applies wet precursor films with ±2% thickness tolerance across full plate dimensions.
Staged Thermal Decomposition: Multi-zone furnace treatment pyrolyzes precursors between 420°C and 520°C under controlled partial oxygen atmospheres.
Final Stress-Relief Recrystallization: A high-temperature post-cure step at 480°C for 2 hours locks the solid-solution crystalline lattice while relieving interfacial thermal strain.
This protocol produces an engineered "mud-crack" morphology. Micro-fissures (widths < 0.5 μm) distribute surface tension during rapid gas evolution, preventing coating spallation under high-current industrial cycling.
Selecting the proper coating system requires matching the active formulation to the chemical matrix of your electrolysis cells.
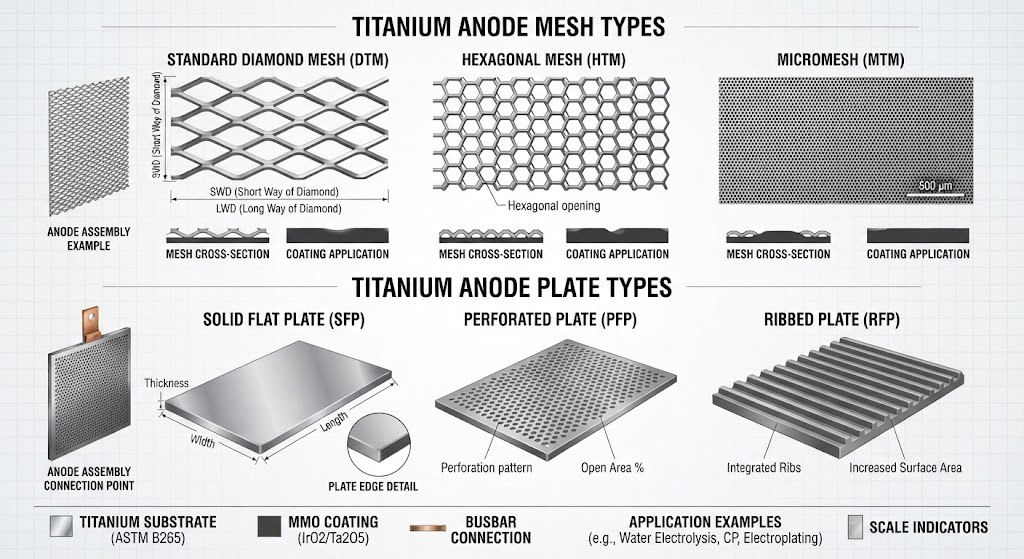
Standard chlor-alkali membrane cells and seawater electrochlorination units operate with high halide concentrations (NaCl > 25 g/L). For these setups, specify Ru-Ir coated titanium expanded mesh anode substrates. The RuO2 component delivers low CER overpotential, minimizing electricity consumption per kilogram of equivalent active chlorine generated.
Electrowinning electrolytes contain high sulfuric acid concentrations (150–220 g/L H2SO4) alongside trace dissolved fluorides or manganese. In this environment, Ru-Ir coatings fail within 90 days due to ruthenium dissolution. Heavy-duty ASTM B265 Grade 1 titanium plates activated with IrO2-Ta2O5 coatings (20–25 g/m² noble metal) deliver 3 to 6 years of continuous service life in acid electrowinning tanks.
Electrodeposited copper foil manufacturing demands extreme dimensional stability and consistent cross-width current distribution at high current densities (> 8,000 A/m²). Ir-Ta formulations combined with precision CNC titanium machined anode assemblies maintain radial tolerances within ±0.3 mm, preventing edge-burning and non-uniform foil grain structures.
Standard binary coatings often fail prematurely in complex electrolytes where multiple competitive reactions occur simultaneously.
Industrial wastewater or complex hydrometallurgical leaches often contain 5–15 g/L Cl⁻ alongside 50–100 g/L SO42-. In these systems, standard Ru-Ir coatings degrade from oxygen attack, while Ir-Ta coatings suffer localized pitting. China Titanium Factory addresses this by applying a Quaternary Ru-Ir-Sn-Pt Hybrid Coating.
SnO2 Doping: Increases the electrical conductivity of the oxide film and stabilizes the rutile lattice.
Platinum Interlayer: Provides an electrochemical backstop, maintaining low contact resistance if surface micro-cracks form.
Fluoride concentrations as low as 5–10 ppm dissolve the native protective TiO2 passive layer underneath the coating, causing catastrophic spallation. For fluoride-bearing environments, we apply a dense 10 μm Thermal Tantalum-Iridium Diffusion Barrier Interlayer directly to the Grade 1 titanium before applying the MMO catalytic topcoat.
An MMO anode's service life depends heavily on the purity and surface preparation of its underlying titanium substrate. We utilize exclusively high-ductility, low-interstitial Grade 1 unalloyed titanium (UNS R50250) conforming to ASTM B265, ASTM B348, and ASTM B338.
| Element / Property | ASTM B265 Grade 1 Limit | China Titanium Factory QA Standard |
|---|---|---|
| Iron (Fe) wt% | ≤ 0.20% | ≤ 0.05% (Minimizes localized galvanic pitting) |
| Oxygen (O) wt% | ≤ 0.18% | ≤ 0.10% (Enhances cold ductility during mesh expansion) |
| Hydrogen (H) wt% | ≤ 0.015% | ≤ 0.005% (Prevents thermal hydride embrittlement) |
| Flatness Tolerance | ± 3.0 mm/m² | ± 0.3 mm/m² (Laser flattened for tight inter-electrode gaps) |
Every production batch includes full documentation: EN 10204 Type 3.1 Mill Test Certificates (MTC), non-destructive X-Ray Fluorescence (XRF) coating loading analysis, and Accelerated Life Testing (ALT) logs run according to national chemical standard HG/T 2471-2017.
Procurement choices should balance initial acquisition costs with total life-cycle power consumption and replacement schedules. Electricity accounts for roughly 70–85% of total operating expenses in industrial electrochemical processes.
A reduction of just 100 mV in cell overpotential through an optimized catalytic coating delivers substantial operational savings. In a 50 kA electrowinning cell line operating 8,000 hours per year at 0.08/kWh, a 100 mV drop saves approximately32,000 annually per cell bank in electrical power.
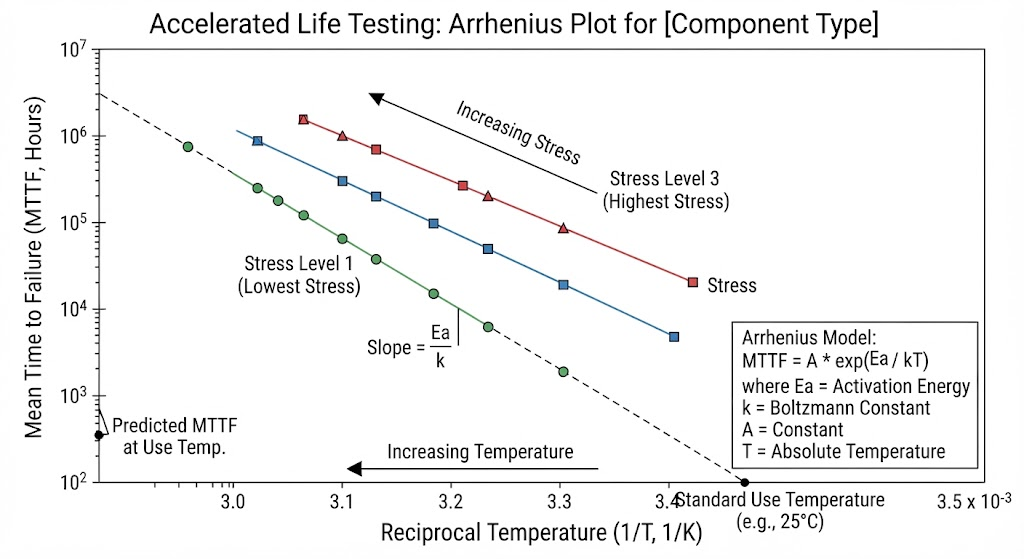
Under-specifying noble metal loading (e.g., choosing 6 g/m² instead of 15 g/m² to reduce upfront cost) shortens anode lifespan exponentially. In high current applications, saving 15% on initial anode procurement can double overall operational costs due to unplanned plant downtime and recoating turnarounds.
Ru-Ir coatings feature lower initial procurement costs because ruthenium is less expensive than iridium and tantalum. In neutral or alkaline brine systems (chlor-alkali, pool chlorination, seawater cells), Ru-Ir yields the lowest TCO. However, if oxygen evolution occurs in acidic conditions (pH < 4), Ru-Ir degrades within 3 to 6 months due to ruthenium dissolution. In acidic, sulfate-rich environments, Ir-Ta coated titanium anodes provide 3 to 5 years of stable operation, lowering overall lifecycle costs per hour by more than 45%.
China Titanium Factory supplies a 3-tier quality verification dossier with every shipment:
X-ray Fluorescence (XRF) Report: Validates precise noble metal loading per square meter (g/m² for Ru, Ir, Ta, Pt).
SEM & EDS Analysis: High-resolution cross-sectional imaging verifying crystalline solid-solution structure and crack morphology.
EN 10204 Type 3.1 Traceability: Complete mechanical and chemical mill certification for the Grade 1 titanium base substrate.
Yes. Because the titanium base metal remains structurally intact after electrochemical service, substrates can be refurbished. China Titanium Factory removes spent residual oxide films via chemical stripping, re-etches the anchor profile to ASTM standards, and reapplies fresh MMO coatings, restoring the anode to original specifications at roughly 40–60% of the cost of a new assembly.
Premature failure typically results from three conditions: operating above critical breakdown current densities, the presence of trace contaminants (such as fluorides > 5 ppm or non-conductive organic siloxanes), or continuous current reversal without a polarity-reversal-rated MMO formulation. Current reversals drive cathodic hydride embrittlement on unprotected titanium, causing rapid coating delamination.
China Titanium Factory operates an integrated manufacturing facility combining titanium sponge melting, precision sheet/mesh processing, CNC fabrication, and automated MMO coating lines.
Submit Design Specifications: Send your CAD drawings (.DWG, .STEP, .PDF) alongside your operating parameters (electrolyte chemistry, temperature, pH, current density, target lifespan).
Receive Engineering DFM & Sizing Dossier: Within 4 hours, our electrochemical engineering team delivers a comprehensive review covering substrate profile, coating composition, target loading (g/m²), and voltage efficiency modeling.
Sample Dispatch & Production Scale-Up: Custom test coupons or sample meshes ship within 5 working days, supported by our direct technical engineering team.



Contact Us
Room 21003, 10th Floor, Unit 2, Building 1, Xianning International Plaza, No.29 Xianning West Road, Beilin District, Xi'an City
Copyright © Xi'an Shiguang Jingyan Technology Co., Ltd. All Rights Reserved.