Titanium Square Tubing: Engineering Excellence & Sourcing
Titanium square tubing is an advanced structural hollow section (HSS) engineered for high-stress, weight-critical, and highly corrosive operating environments. Combining high specific tensile strength (up to 1,000 MPa in alloyed grades) with a density roughly 45% lower than structural steel (4.43–4.51 g/cm³), these box profiles deliver superior torsional stiffness, structural stability, and absolute resistance to chloride-induced pitting. Manufactured to strict global standards including ASTM B861 and AMS 4943, precision hollow sections are the structural foundation for advanced aerospace frameworks, subsea housings, and high-performance racing platforms.
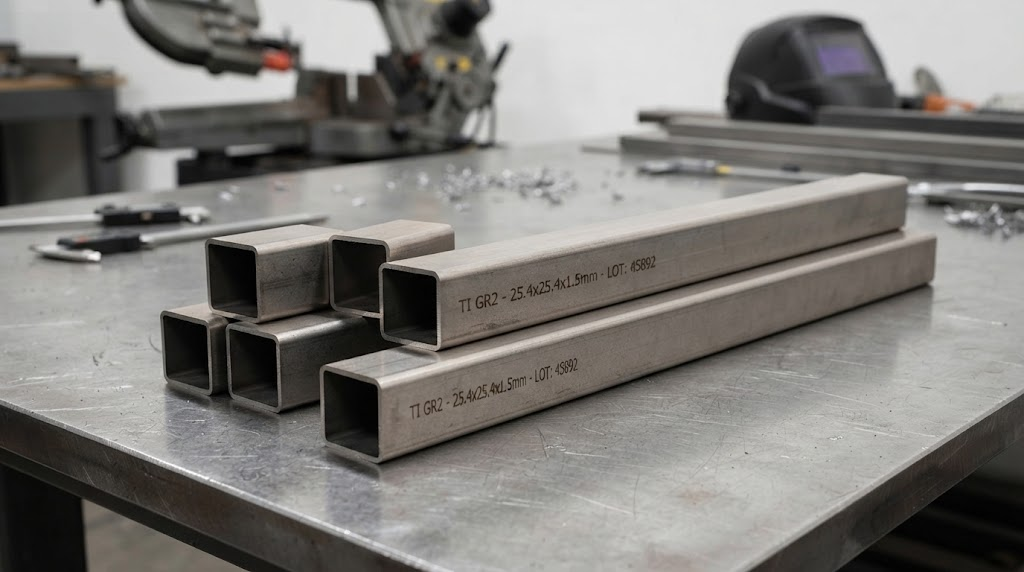
When selecting structural geometries, the square cross-section offers uniform moments of inertia across both the X and Y axes. This geometry eliminates the directional buckling vulnerabilities inherent in open profiles like channels or I-beams.
At China Titanium Factory, we integrate vacuum arc remelting (VAR), precision hot extrusion, and specialized squaring dies. This end-to-end control delivers uniform wall thickness and tight corner radii for mission-critical structural systems.
Material Grades & Mechanical Property Benchmarks
Selecting the proper alloy grade depends on the operating balance between yield strength, elongation, formability, and operating temperature. In our facility, we produce titanium box profiles across commercially pure (CP) and alpha-beta alloy systems.
| Grade / Alloy | Tensile Strength (MPa) | Yield Strength 0.2% (MPa) | Elongation (% in 50mm) | Elastic Modulus (GPa) | Density (g/cm³) |
|---|---|---|---|---|---|
| Grade 2 (UNS R50400) | ≥ 345 | 275 – 450 | ≥ 20 | 105 | 4.51 |
| Grade 5 Ti-6Al-4V Material Profile | ≥ 895 | ≥ 828 | ≥ 10 | 114 | 4.43 |
| Grade 9 / 3Al-2.5V (UNS R56320) | ≥ 620 | ≥ 483 | ≥ 15 | 107 | 4.48 |
| Grade 7 (0.15% Pd Alloy) | ≥ 345 | 275 – 450 | ≥ 20 | 105 | 4.51 |
Grade Selection Criteria
Grade 2 Titanium Box Section: The standard choice for chemical processing, marine framing, and exhaust components. It offers high cold ductility, clean weldability, and resistance to wet chlorine and sea-water environments.
Grade 5 (Ti-6Al-4V) Square Tubing: The premier structural aerospace alloy. Yield strengths exceed 828 MPa, making it ideal for high-stress space frame structures, motorsport impact zones, and subsea chassis.
Grade 9 (Ti-3Al-2.5V) Tubing: An alloy combining 70% higher strength than CP Grade 2 with excellent cold-forming capabilities. It is common in aerospace hydraulic lines, bicycle frames, and lightweight marine masts.
Manufacturing Standards, Dimensional Sizing, and Tolerances
China Titanium Factory manufactures titanium square tubing across a broad dimensional matrix. We maintain tight compliance with international aerospace and industrial standards.
| Parameter | Standard Sizing Range | Custom Sizing Range | Standard Tolerance |
|---|---|---|---|
| Outer Width & Height (A x B) | 10 x 10 mm to 100 x 100 mm | Up to 200 x 200 mm | ± 0.10 mm to ± 0.40 mm |
| Wall Thickness (WT) | 0.8 mm to 6.0 mm | 0.5 mm to 12.0 mm | ± 8% to ± 10% |
| Corner Radius ($R_{ext}$) | 1.5 × WT to 2.5 × WT | Sharp corner ($R < 1.0 × WT$) | ± 0.25 mm |
| Straightness Deviation | ≤ 1.5 mm / 1000 mm | ≤ 0.8 mm / 1000 mm (Precision) | Precision Class DIN EN 10305 |
| Twist Angle / Meter | ≤ 1.0° per meter | ≤ 0.5° per meter | ASTM B861 Spec |
Applicable International Material Standards
ASTM B861: Standard Specification for Titanium and Titanium Alloy Seamless Pipe and Tube.
ASTM B338: Seamless and Welded Titanium and Titanium Alloy Tubes for Condensers and Heat Exchangers.
ASTM B862: Standard Specification for Titanium and Titanium Alloy Welded Pipe.
AMS 4943 / AMS 4944: Aerospace Material Specification for Ti-3Al-2.5V seamless hydraulic and structural tubing.
DIN 17860 / EN 10204: European standard mapping material quality and inspection documentation rules.
Seamless vs. Welded (ERW) Titanium Square Tube Manufacturing
Deciding between seamless and welded titanium hollow structural sections requires balancing mechanical loading limits, internal hydraulic/pneumatic pressures, and production costs.
1. Seamless Extrusion & Cold Pilgering
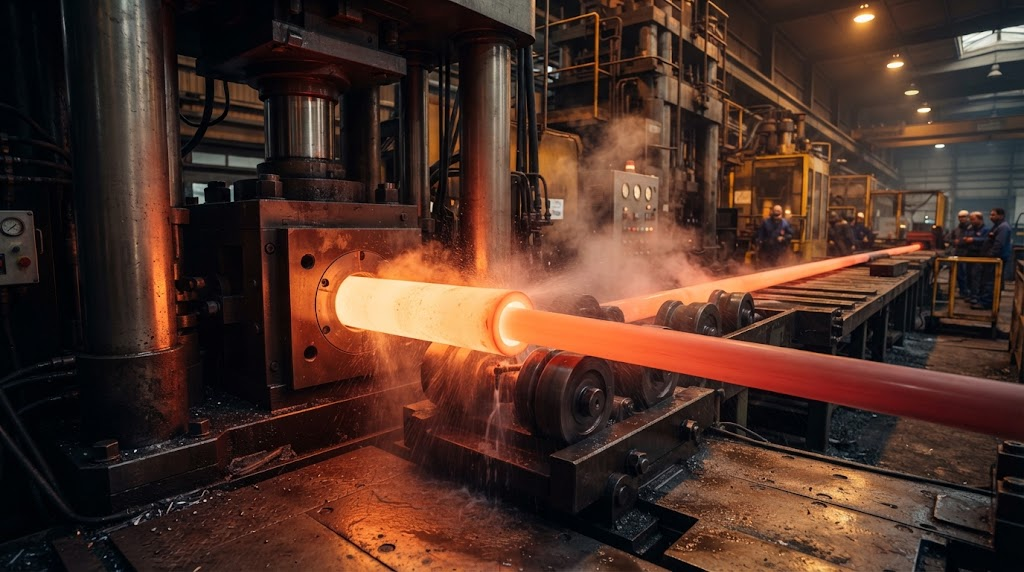
Seamless square tubing begins as a solid billet drilled and hot-extruded into a mother tube. We process this preform through multi-axis cold pilger mills and cold drawing dies over precision mandrels to square the cross-section.
Structural Integrity: 100% monolithic wall microstructure with zero Heat Affected Zone (HAZ).
Pressure Performance: Burst pressures match full hoop strength limits without joint-efficiency derating ($E = 1.0$). Learn more about our high-pressure manufacturing on our Titanium Seamless Tubing product page.
Applications: Subsea pressure housings, aerospace structural spars, and chemical plant high-pressure conduits.
2. Roll-Formed and Welded (TIG / Laser)
Welded square tubing is formed continuously from cold-rolled titanium strip passing through precision roll-forming clusters, sealed via automated GTAW or High-Power Fiber Laser welding in an inert trailing chamber, and sized through squaring calibration rolls.
Wall Uniformity: Tight concentricity tolerances with consistent wall gauge (±0.05 mm) along entire structural runs.
Surface Finish: Internal and external roughness average down to $Ra \le 0.4\,\mu\text{m}$.
Cost Efficiency: Higher material yield and reduced tooling overhead across standard architectural, exhaust framing, and decorative projects.
The CTF Quad-Forming™ Protocol: Precision Squaring & Quality Assurance
Cold-forming titanium into precise square profiles without inducing tensile cracking on outer radii requires proprietary metallurgical control. China Titanium Factory uses the CTF Quad-Forming™ Protocol across our production lines.
Controlled Vacuum Recrystallization: Mother tubes undergo intermediate vacuum annealing at $680^\circ\text{C} \pm 5^\circ\text{C}$ ($10^{-3}\,\text{Pa}$ vacuum) to homogenize grain structure to ASTM Grain Size No. 7.5 or finer, removing residual work hardening.
Multi-Pass Precision Squaring: Tubes advance through a 4-roller driven calibration stand with incrementally decreasing profile radii ($R/t$). This distributes compressive deformation evenly and prevents wall thinning on the flats.
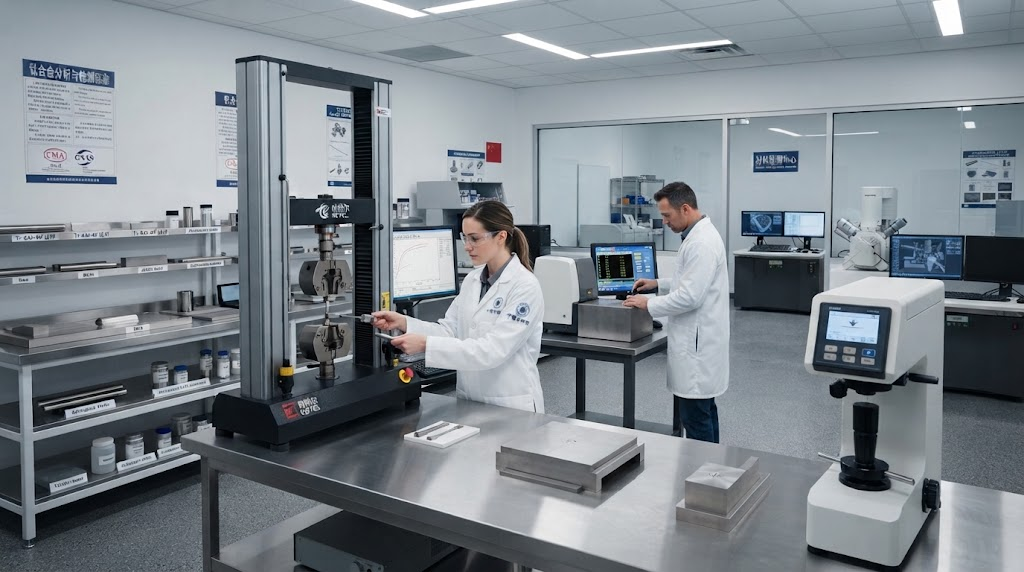
In-Line Non-Destructive Testing (NDT): Every linear meter is inspected via 360° encircling-coil Eddy Current (ET) per ASTM E426 and Ultrasonic Testing (UT) per ASTM E213 to identify internal micro-voids, inclusions, or surface tears down to 0.05 mm depth.
Dimensional Laser Verification & MTR Issuance: Finished tubes are scanned using a 4-axis multi-point laser micrometer to log wall thickness, convex/concave deviation, and angular orthogonality. We pair every batch with full Mill Test Certifications & Quality documentation conforming to EN 10204 3.1.
Industrial Applications & Engineering Case Studies
1. Aerospace & Defense Structural Frameworks
Grade 5 and Grade 9 square tubes serve as internal cross-bracing and equipment mounting frames for satellite buses, payload bays, and drone airframes. The rectangular surfaces simplify fastener mounting compared to round tubes, eliminating expensive machined saddle interfaces.
2. High-Performance Motorsport & Supercars
Chassis builders use Grade 2 and Grade 5 box sections for rear crash structures, suspension arms, and Titanium Exhaust Components. Titanium's fatigue threshold prevents cyclic failure under heavy track vibrations while shaving critical kilograms from the chassis center of gravity.
3. Marine & Offshore Subsea Engineering
Unalloyed titanium box sections are immune to pitting and crevice corrosion in warm, oxygenated seawater ($>30^\circ\text{C}$). Oceanographic teams build autonomous underwater vehicle (AUV) frameworks, offshore instrumentation rigs, and marine sensor cages directly from Grade 2 box tubing.
4. Chemical Processing & Electroplating Racks
Grade 2 and Grade 7 square tubes form rigid, conductive support racks inside aggressive acid baths (hydrochloric, nitric, chromic acids). The square geometry provides flush contact planes for cathode/anode bar bolting, lowering electrical contact resistance.
Fabrication, Bending, and TIG Welding Engineering Guidelines
Secondary processing of titanium square tubing requires strict engineering rules to avoid interstitial gas contamination and preserve dimensional accuracy.
Cold Bending & Springback Compensation
Because titanium's elastic modulus is roughly half that of carbon steel (~105 GPa vs ~205 GPa), cold bending produces significant elastic springback. To bend square tubing successfully:
Minimum Centerline Radius ($CLR$): For CP Grade 2, maintain $CLR \ge 2.5 \times \text{Width}$. For Grade 5 (Ti-6Al-4V), ensure $CLR \ge 4.0 \times \text{Width}$ or switch to warm bending at $500^\circ\text{C}$ to $600^\circ\text{C}$.
Tooling Setup: Use a multi-ball internal mandrel combined with a zero-clearance bronze wiper die to prevent flat-face collapsing and outside-corner thinning.
Springback Overbend: Overbend by 8° to 14° depending on wall-thickness-to-width ratio ($t/W$).
GTAW / TIG Welding Protocols
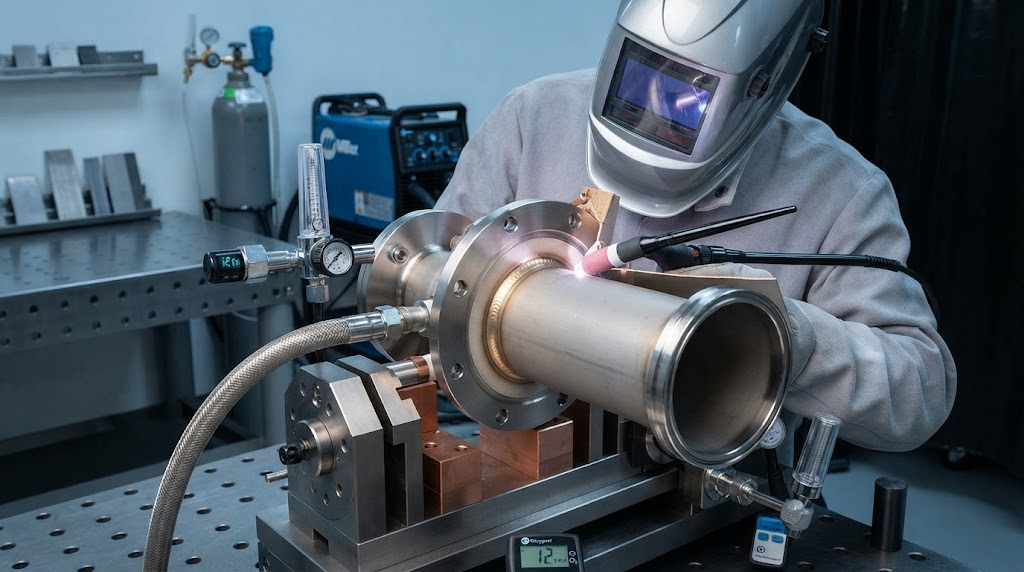
Titanium readily absorbs oxygen, nitrogen, and hydrogen at temperatures above $400^\circ\text{C}$, causing severe embrittlement. Structural joint welding must follow these parameters:
Shielding Atmosphere: Use ultra-high-purity Argon (≥ 99.999% purity, dewpoint ≤ -65°C).
Torch, Trailing Shield & Back-Purge: A gas lens torch must be paired with an extended trailing shield and a positive internal back-purge box. Keep root purge oxygen levels below 50 ppm before striking an arc.
Post-Weld Visual Inspection: The weld seam must exhibit a bright silver or light straw color. Dark straw/blue indicates moderate oxidation; grey or white powdery deposits indicate severe contamination and require scrapping the joint per AWS G2.4/G2.4M standards.
B2B Procurement, Custom OEM Sizing, and RFQ Process
China Titanium Factory maintains warehouse stock in standard dimensions while engineering custom-profile box sections for specialized OEM applications.
OEM Capabilities & Sourcing Benefits
Custom Dies: Rapid tooling production for non-standard rectangular or trapezoidal cross-sections within 15 working days.
Cut-to-Length Precision: Burr-free CNC cold sawing and multi-axis wire-cut EDM down to ±0.2 mm length tolerance.
Export Packaging: Export-grade fumigated wooden crates with individual PVC sleeve tubing wraps to eliminate surface abrasion during intermodal sea and air transit.
Full Traceability: Complete chemical heat analysis, mechanical tensile test reports, and non-destructive examination logs shipped with every delivery.
Request a Fast Wholesale Quote on Titanium Square Tubing
Access direct mill pricing, certified aerospace and commercial grade alloys, and custom sizing options delivered worldwide.
Submit Your Sourcing SpecificationsFrequently Asked Questions About Titanium Square Tubing
How is the theoretical weight of titanium square tubing calculated?
Use the structural box formula based on material density ($\rho \approx 4.51\,\text{g/cm}^3$ for Grade 2):
$$\text{Weight (kg/m)} = 4 \times \text{Thickness (mm)} \times (\text{Width (mm)} - \text{Thickness (mm)}) \times 0.00451$$
For Grade 5 (Ti-6Al-4V), adjust the calculation factor to 0.00443.
Can China Titanium Factory produce square tubing with sharp, 90-degree internal and external corners?
Yes. While standard squaring dies form an external corner radius of $1.5 \times WT$, we use specialized multi-pass drawing dies and wire EDM shaving to produce sharp-corner profiles ($R < 0.5\,\text{mm}$) for architectural, vacuum seal, and optical chassis applications.
What weld discoloration is acceptable on titanium square tubing?
Bright silver indicates perfect inert atmospheric shielding. Light straw/gold is metallurgically acceptable across industrial standards. Blue, purple, grey, or chalky white indicate atmospheric contamination (interstitial absorption) that degrades fatigue performance and ductility.
What is the Minimum Order Quantity (MOQ) and production lead time?
For stocked standard metric sizes (e.g., 20x20mm, 25.4x25.4mm, 50x50mm in Gr 2 / Gr 5), the MOQ is 10 meters with 3-day dispatch. Custom mill production runs or non-standard profiles generally require a 50 kg MOQ with a 2 to 4-week lead time.