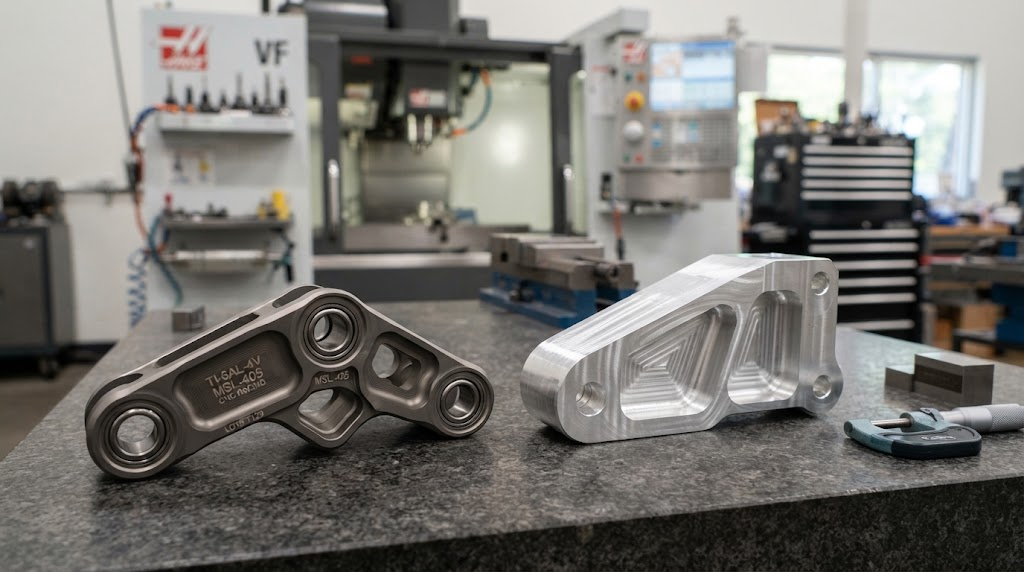
An aerospace titanium manufacturer produces flight-critical, high-integrity titanium mill products and forgings engineered to withstand extreme cyclical mechanical fatigue, elevated aerodynamic temperatures, and corrosive flight environments. Qualified production requires AS9100D certified quality systems, multi-stage vacuum melting to eliminate interstitial defects, and full compliance with international material standards such as AMS, ASTM, Boeing BMS, and Airbus ASN-A specifications.
At China Titanium Factory (chinatitaniumfactory.com), our integrated manufacturing infrastructure operates under stringent aerospace quality management protocols. We convert high-purity virgin sponge titanium into precision-engineered ingots, forged billets, plates, sheets, rolled rings, and close-tolerance bars tailored for mission-critical aerostructures, jet engines, and space vehicle propulsion systems.
Our mill infrastructure couples multi-stage Vacuum Arc Remelting (VAR) and Electron Beam Cold Hearth Remelting (EBCHR) with high-tonnage multi-directional forging presses. This fully integrated processing pipeline guarantees complete lot-to-lot traceability, microstructural homogeneity, and zero melt defect propagation across global Tier-1 and Tier-2 aviation supply chains.
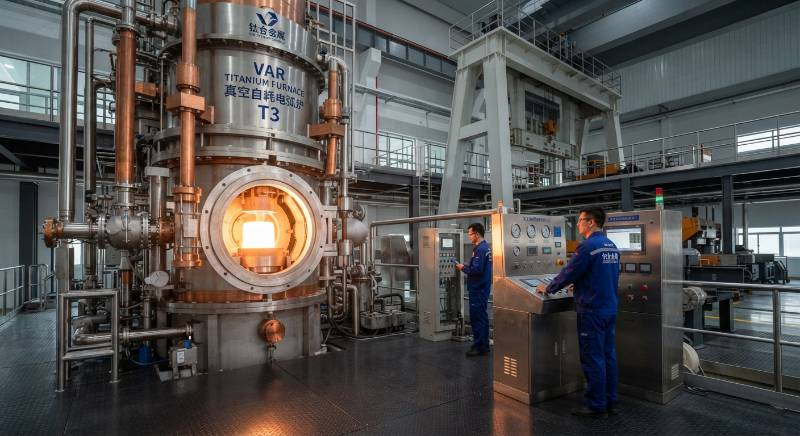
Melt integrity dictates the structural reliability of rotating aerospace components and high-stress airframe joints. In rotating turbine discs, a single microscopic defect can act as a stress concentration site, accelerating low-cycle fatigue failure.
Aerospace-grade ingot preparation demands the complete elimination of two destructive metallurgical anomalies:
High-Density Inclusions (HDIs): Refractory metal contaminants (such as tungsten, tantalum, or molybdenum carbide particles) originating from tool wear or contaminated master alloys. Their high melting point prevents full dissolution in standard single-melt setups.
Low-Density Inclusions (LDIs / Hard Alpha): Nitrogen-rich or oxygen-rich interstitial segregations characterized by high hardness, extreme brittleness, and an elevated local beta transus temperature (βtr).
Hard Alpha Inclusion (LDI): An interstitial-rich α-phase anomaly possessing high nitrogen or oxygen concentrations, exhibiting local microhardness exceeding 500 HV compared to ~320 HV for standard Ti-6Al-4V matrix, rendering it prone to micro-cracking under flight load.
To eliminate these risks, China Titanium Factory enforces a mandatory Double VAR or Triple VAR melting sequence for primary structural applications, alongside EBCHR + VAR melting for premium rotating components.
| Melting Route | Refining Mechanism | LDI / HDI Removal Efficacy | Primary Aerospace Target |
|---|---|---|---|
| Double VAR | Vacuum degassing & controlled directional solidification | Standard baseline; removes volatile interstitials | Static airframe structures (AMS 4911, AMS 4928) |
| Triple VAR | Extended molten exposure; total dissolution kinetics | Near-complete dissolution of nitrogen-rich clusters | Rotorcraft dynamic components, engine compressor discs |
| EBCHR + VAR | Cold-hearth physical settling & high-vacuum surface evaporation | Complete gravitational separation of HDIs; thermal dissolution of LDIs | Critical jet engine rotating hardware, landing gear forgings |
Purity starts at the reduction stage. We utilize strictly certified 0A-grade small-particle virgin sponge titanium sourced via the Kroll process.
Dissolved interstitial gases directly shift the alloy's phase boundaries. Oxygen and nitrogen act as potent α-stabilizers, raising the β-transus temperature and degrading fracture toughness if unconstrained.
Oxygen (O): Strictly constrained to ≤ 0.13 wt% for Grade 23 (ELI) and ≤ 0.20 wt% for Grade 5 standard.
Nitrogen (N): Held below 0.02 wt% (≤ 200 ppm) to prevent local hard alpha nucleation.
Hydrogen (H): Maintained ≤ 0.0125 wt% (≤ 125 ppm); vacuum degassing ensures post-anneal levels remain below 50 ppm to prevent subcritical hydrogen-induced delayed cracking.
Carbon (C): Limited to ≤ 0.05 wt% to eliminate grain boundary titanium carbide (TiC) precipitation.
To deliver uniform microstructures and zero defects across heavy sections, China Titanium Factory enforces a proprietary manufacturing methodology: The CTF AeroPure™ Ingot-to-Component Quality Protocol.
This 5-stage framework governs every mill operation from raw sponge validation to final non-destructive testing:
Stage 1: Raw Stock Characterization & Homogenized Master Blending: 100% spectrographic verification of virgin 0A sponge, pure aluminum, and high-purity vanadium-aluminum master alloy compacts.
Stage 2: Multiphase Vacuum Melting (EBCHR/Triple VAR): Precise melt-rate feedback control prevents ingot pipe formation and suppresses center-line segregation of alloying elements like β-stabilizing vanadium.
Stage 3: Sub-Transus Cogging & High-Ratio Forging (>4:1): Heavy open-die break-down forging operating through the β and α+β fields, establishing fine, equiaxed α-globules within a transformed β-matrix.
Stage 4: Automated Heat Treatment & Quench Dynamics: Computer-controlled Solution Treating and Aging (STA) or Mill Annealing cycles with uniform furnace thermometry (±5°C conforming to AMS 2750 pyrometry standards).
Stage 5: Dual-Channel Nadcap-Accredited NDT: 100% Class A / Class AA automated immersion ultrasonic scanning paired with high-sensitivity macro-etch inspection for surface structural continuity.
Engineering Insight: Achieving high low-cycle fatigue (LCF) resistance requires achieving a fine bimodal microstructural condition. In our cogging lines, applying deformation reduction ratios exceeding 4:1 below the β-transus converts coarse lamellar structures into uniform 3–5 μm primary equiaxed α grains, maximizing both yield strength and crack propagation resistance.
Modern airframe and engine architectures leverage distinct metallurgical classes of titanium alloys to optimize weight, fracture mechanics, and thermal envelope stability.
According to research cataloged by the ASM International Materials Information Society, alpha-beta and near-beta titanium alloys account for over 70% of structural titanium consumption in modern wide-body commercial aircraft.
| Alloy Grade | Phase Class | Nominal Composition | Yield Strength (MPa) | Tensile Strength (MPa) | Key Aerospace Applications |
|---|---|---|---|---|---|
| Ti-6Al-4V (Gr 5) | α + β | Ti-6.0Al-4.0V-0.18O | ≥ 828 | ≥ 895 | Fuselage bulkheads, wing spars, engine mounts |
| Ti-6Al-4V ELI (Gr 23) | α + β (Extra Low Interstitial) | Ti-6.0Al-4.0V-0.13O | ≥ 795 | ≥ 860 | Cryogenic propellant tanks, space structures, rotor hubs |
| Ti-5553 | Near β | Ti-5Al-5Mo-5V-3Cr | ≥ 1160 (STA) | ≥ 1240 (STA) | Heavy landing gear forgings, pylon attachments |
| Ti-10-2-3 | Near β | Ti-10V-2Fe-3Al | ≥ 1105 | ≥ 1190 | High-strength landing gear trucks, rotor mast links |
| Ti-6246 | α + β (High Temp) | Ti-6Al-2Sn-4Zr-6Mo | ≥ 1070 | ≥ 1170 | Intermediate gas turbine compressor discs and impellers |
| TiAl (Gamma) | Intermetallic | Ti-48Al-2Cr-2Nb | ≥ 450 (at 650°C) | ≥ 550 (at 650°C) | Low-pressure turbine (LPT) blades, exhaust valves |
China Titanium Factory manufactures all products under direct equivalence to prime airframe and propulsion material specifications.
| Material Form | SAE / AMS (USA) | ASTM Standard | Boeing Standard | Airbus Standard | European / DIN |
|---|---|---|---|---|---|
| Ti-6Al-4V Sheet / Plate | AMS 4911 | ASTM B265 (Gr 5) | BMS 7-348 Cl 1 | ASN-A 3307 | DIN 3.7164.1 / EN 3456 |
| Ti-6Al-4V Bar / Billet | AMS 4928 | ASTM B348 (Gr 5) | BMS 7-348 Cl 2 | ASN-A 3308 | DIN 3.7164.2 / EN 3457 |
| Ti-6Al-4V ELI (Cryogenic) | AMS 4907 / AMS 4930 | ASTM B265/B348 (Gr 23) | BMS 7-348 Cl 3 | ASN-A 3310 | DIN 3.7164.7 / EN 3465 |
| Ti-6Al-4V Forgings | AMS 4965 / AMS 4967 | ASTM B381 (F-5) | BMS 7-348 Type 4 | ASN-A 3312 | EN 3468 |
| Ti-3Al-2.5V Hydraulic Tube | AMS 4943 / AMS 4945 | ASTM B338 (Gr 9) | BMS 7-234 | ASN-A 3268 | DIN 3.7194 / EN 3314 |
China Titanium Factory operates dedicated open-die hydraulic forging presses up to 10,000 metric tons, coupled with multi-axis CNC high-speed ring rolling systems. We engineer customized macro-grain flow lines that align with principal stress vectors in finished aerospace components.
Our comprehensive forging operations encompass:
Open-Die Cogging & Billet Production: Controlled high-strain reduction forging down to uniform round, octagonal, and rectangular billets with minimal center porosity.
Precision Closed-Die Forging: Near-net shape forming of structural fittings, landing gear torque links, and engine mount pylons, delivering buy-to-fly ratio improvements up to 40%.
Isothermal / Hot-Die Forging: Die tooling maintained at work-piece temperature under protective atmosphere for processing crack-sensitive near-beta and intermetallic titanium alloys.
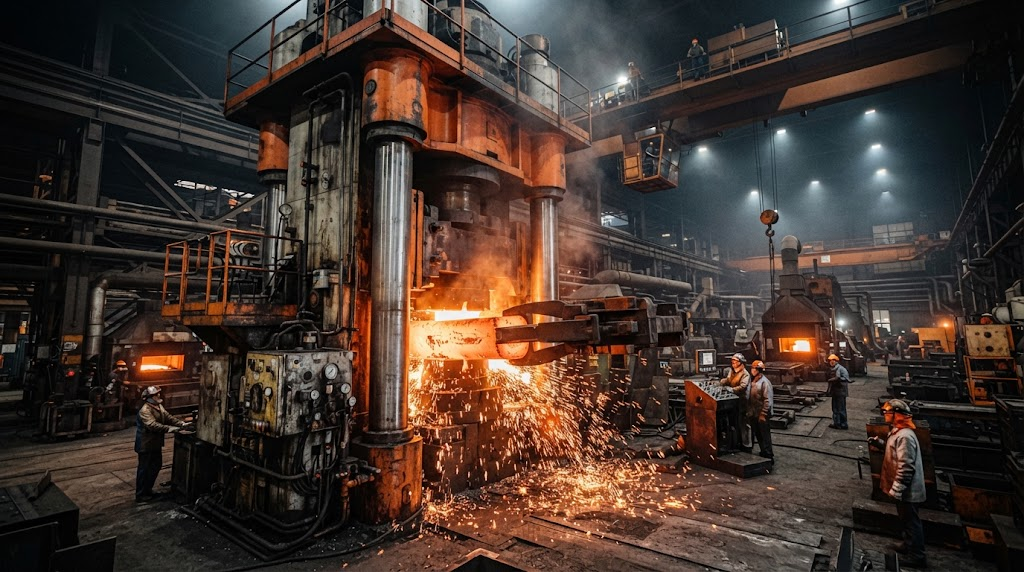
We manufacture seamless rolled titanium rings designed to operate under severe thermal gradient cycles and rotational burst loads.
Our radial-axial CNC ring rolling cell produces seamless rings from 300 mm up to 4,500 mm outer diameter, with maximum face heights of 650 mm. Applications include:
Fan containment casings and fan stator rings (Ti-6Al-4V).
Intermediate compressor stage rings and disc blanks (Ti-6242 / Ti-6246).
Turbine exhaust and nacelle attachment flanges.
China Titanium Factory maintains tight dimensional controls, flat tolerances, and smooth surface conditioning across our full product range.
| Product Format | Standard Specs | Dimensional Range | Dimensional Tolerance | Surface Condition |
|---|---|---|---|---|
| Aerospace Plates | AMS 4911, BMS 7-348 | Thickness: 6.0 mm – 150.0 mm Width: Up to 3,000 mm Length: Up to 10,000 mm | AMS 2242 Tightened (± 0.38 mm to ± 1.20 mm) | Descaled, acid pickled, or precision waterjet milled; Ra ≤ 3.2 μm |
| Precision Sheets | AMS 4911, MIL-T-9046 | Thickness: 0.5 mm – 4.76 mm Width: Up to 1,250 mm Length: Up to 3,500 mm | AMS 2242 Class A (± 0.05 mm to ± 0.15 mm) | Cold-rolled, bright annealed, chemically etched; Ra ≤ 0.8 μm |
| Forged Billets & Bars | AMS 4928, AMS 4967 | Diameter: Ø 10 mm – Ø 450 mm Length: Up to 6,000 mm | h8, h9, h11 or centerless ground (±0.02 mm) | Centerless ground, peeled, turned; 100% UT Class A/AA |
| Seamless Hydraulic Tubes | AMS 4943, AMS 4945 | OD: 3.18 mm – 50.8 mm WT: 0.40 mm – 3.0 mm | AMS 2244 Special (± 0.05 mm OD/WT) | Cold drawn, vacuum stress relieved, pickling passivated |
| Fastener Wire & Coils | AMS 4967, AMS 4928 | Diameter: Ø 1.5 mm – Ø 12.0 mm | h7 / h8 high precision | Eddy-current tested, cold-heading lubricant coated |
Design and structural calculations for aerospace airframes require validated thermo-physical and fracture mechanics metrics.
| Property Parameter | Ti-6Al-4V (Grade 5) | Ti-6Al-4V ELI (Grade 23) | Ti-5553 | Ti-6242 |
|---|---|---|---|---|
| Density (ρ) | 4.43 g/cm³ | 4.43 g/cm³ | 4.65 g/cm³ | 4.54 g/cm³ |
| Elastic Modulus (E) | 114 GPa | 110 GPa | 112 GPa | 117 GPa |
| Beta Transus (βtr) | 995 ± 15 °C | 975 ± 10 °C | 860 ± 10 °C | 995 ± 10 °C |
| Fracture Toughness (KIC) | 55 – 75 MPa√m | 80 – 110 MPa√m | 45 – 65 MPa√m | 60 – 80 MPa√m |
| Thermal Expansion (CTE) | 8.6 × 10⁻⁶ /°C | 8.6 × 10⁻⁶ /°C | 8.2 × 10⁻⁶ /°C | 8.9 × 10⁻⁶ /°C |
| Max Continuous Use Temp | 350 °C | 300 °C | 315 °C | 540 °C |
Our quality management framework is structured around the zero-defect imperatives of civil and defense aviation. All manufacturing facilities operate under AS9100D and ISO 9001:2015 certification.
Every shipment is accompanied by an authenticated EN 10204 Type 3.1 Mill Test Report (MTR), with Type 3.2 third-party verification (e.g., via DNV, Lloyd's Register, or TÜV) available upon request. Mill test certs detail exact melt parameters, quantitative chemical composition (ICP-OES and LECO gas analysis), tensile and yield properties, bend testing, and microstructural phase validation.
Our non-destructive testing (NDT) capabilities conform to international standards such as ASTM International guidelines and include:
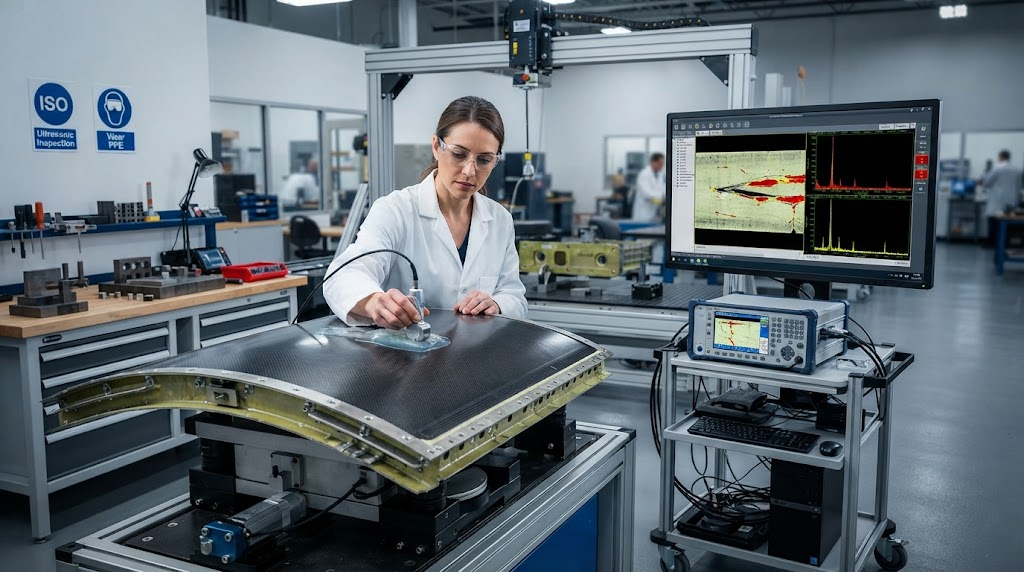
Automated Immersion Ultrasonic Testing (UT): Multi-channel phased array systems calibrated to AMS 2631 Class AA (0.8 mm / #2 FBH equivalent) and Class A (1.2 mm / #3 FBH) standards.
Surface Flaw Inspection: High-sensitivity Fluorescent Liquid Penetrant Inspection (FPI) conforming to ASTM E1417.
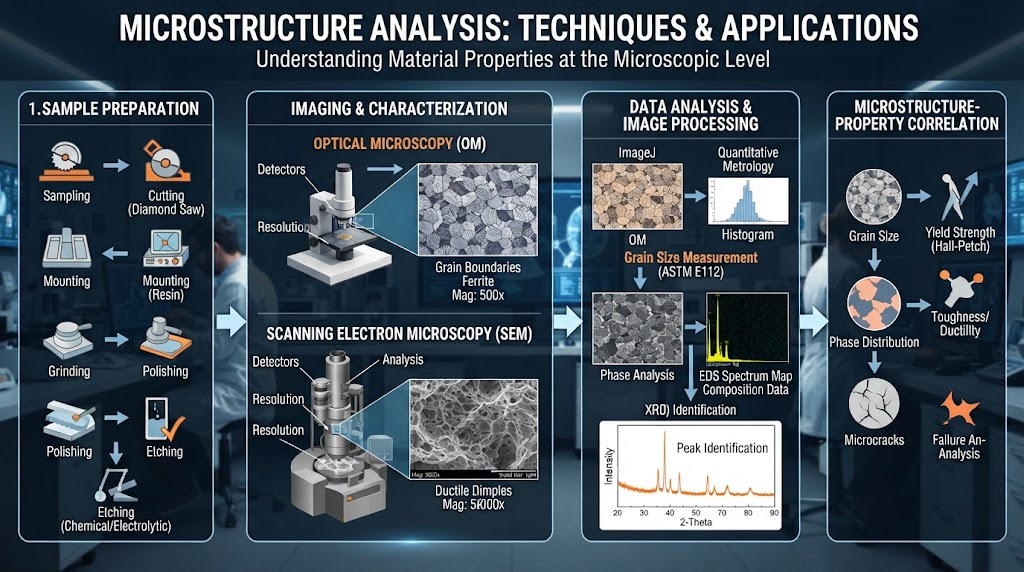
Metallographic Phase Analysis: Alpha case depth evaluation, grain size rating per ASTM E112, and volume fraction determination.
China Titanium Factory manages global trade compliances, providing required dual-use documentation, complete customs tariff classification (HS Code 8108 series), and export packaging engineered to eliminate transit oxidation and corrosion.
Standard aerospace plates and bars from existing inventory ship within 5 to 10 business days. Custom vacuum melt heats, forged billets, and rolled rings requiring bespoke heat treatment cycles typically average 6 to 12 weeks, inclusive of full Nadcap NDT and MTR generation.
While both specifications cover Ti-6Al-4V sheet and plate, AMS 4911 is an aerospace material standard that mandates tighter chemical limits on interstitial gases (such as O, N, and H), specific cross-rolling passes to control microstructural texture, higher room-temperature tensile requirements, and mandatory ultrasonic Class A/AA scanning.
Yes. While our standard delivery includes EN 10204 3.1 mill test certificates, we regularly host independent inspection authorities (such as SGS, TÜV, Bureau Veritas, or customer source inspectors) to perform witness testing and issue validated EN 10204 3.2 certification.
Rotating engine hardware faces severe cyclic fatigue. Triple VAR guarantees the complete thermal dissolution of refractory low-density inclusions (Hard Alpha) and provides extended time for high-density refractory particles to dissolve or settle, eliminating micro-crack initiation sites.
Partner with China Titanium Factory for your flight-critical programs. We provide end-to-end metallurgical consistency, AS9100D quality assurance, complete MTR traceability, and competitive mill-direct pricing.
Request Material Quotation & MTRs


Contact Us
Room 21003, 10th Floor, Unit 2, Building 1, Xianning International Plaza, No.29 Xianning West Road, Beilin District, Xi'an City
Copyright © Xi'an Shiguang Jingyan Technology Co., Ltd. All Rights Reserved.