Titanium is not unconditionally bulletproof in all commercial forms or dimensions, but specialized ballistic-grade alloys engineered to strict metallurgical standards defeat high-velocity projectile threats with exceptional mass efficiency. Defeating a ballistic round requires an armor plate to dynamically dissipate kinetic energy through controlled plastic deformation, high yield strength, and shock wave dispersion without catastrophic structural failure.
When an ogival or conical projectile strikes a metallic armor plate, the collision generates extreme strain rates exceeding 104 s-1 and transient local pressures reaching tens of gigapascals. Ballistic protection is never a binary "yes or no" material property; it is a dynamic equilibrium governed by the projectile's mass, velocity, core composition, impact angle, and the mechanical energy absorption profile of the armor alloy.
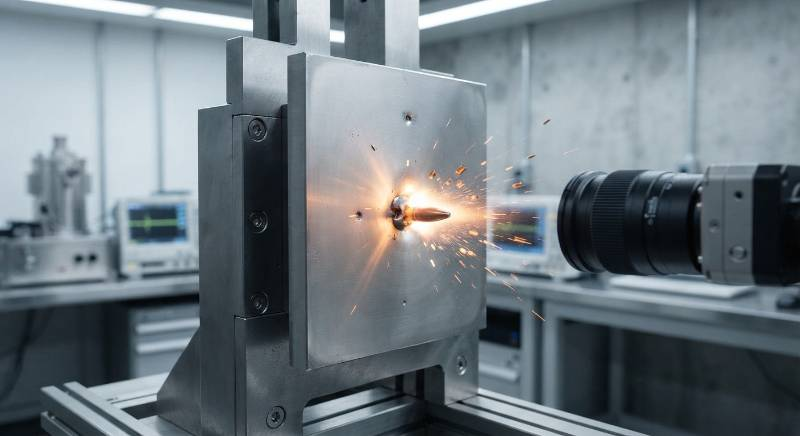
"Ballistic limit velocity (V50) represents the impact velocity at which a specific projectile is predicted to penetrate a target plate 50% of the time, governed rigorously by military specifications such as MIL-DTL-46077."
Unalloyed, commercially pure (CP) titanium (Grades 1 through 4) possesses an unyielding crystalline alpha-phase lattice optimized for corrosion resistance and ductility rather than ballistic impact resistance. CP Grade 2 exhibits a nominal yield strength of approximately 275 to 350 MPa, which permits excessive ductile hole enlargement and deep projectile penetration under rifle fire.
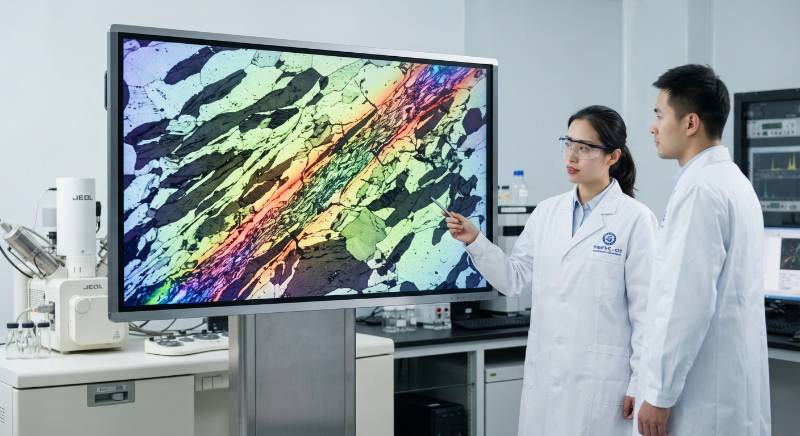
In contrast, the dual-phase alpha-beta structure of Grade 5 Ti-6Al-4V alloy (incorporating 6% aluminum and 4% vanadium) elevates the yield strength beyond 830 MPa and ultimate tensile strength to over 900 MPa. Aluminum stabilizes the alpha phase to enhance lattice hardness and high-temperature strength, while vanadium stabilizes the ductile beta phase to maintain sufficient toughness under dynamic strain rates.
The primary terminal ballistic vulnerability of titanium alloys is adiabatic shear band (ASB) localization. Titanium exhibits low thermal conductivity (approximately 6.7 W/m·K for Ti-6Al-4V versus 50 W/m·K for carbon steel), preventing rapid dissipation of thermal energy generated by high-strain-rate deformation.
During localized projectile penetration, the plastic work converts almost entirely into heat, producing extreme local temperatures exceeding 800°C inside narrow bands (10 to 50 μm wide). This thermal softening outpaces strain hardening, triggering localized plastic instability and "plugging" failure where a cylindrical plug of metal is ejected ahead of the penetrator before the bulk material can fully absorb the projectile's kinetic energy.
Defense engineering and survivability teams do not evaluate armor plates by tensile properties alone. Ballistic procurement requires a multi-dimensional framework balancing dynamic mass efficiency against field operational survivability.
Alloy Metallurgy & Phase Balance: Ensuring an equiaxed, fine-grained alpha-beta microstructure. Standard CP grades fail, while mill-annealed or solution-treated Ti-6Al-4V and Ti-6Al-4V ELI Grade 23 maximize dynamic fracture toughness and resist shear localization.
Adiabatic Shear Band (ASB) Mitigation: Controlling interstitial gas elements (Oxygen < 0.18%, Iron < 0.25%, Hydrogen < 0.0125%) to prevent micro-void coalescence and premature plugging under high-velocity impacts.
Areal Density (AD) Efficiency: Maximizing mass efficiency (Em) relative to Rolled Homogeneous Armor (RHA) steel. Premium titanium armor delivers 30% to 40% weight reductions at equivalent V50 thresholds.
Multi-Hit Durability & Spall Suppression: Retaining structural load-bearing capability following adjacent kinetic impacts without shattering or generating lethal internal spall fragments.
Standardized Ballistic Certification: Sourcing material manufactured and verified strictly in compliance with MIL-DTL-46077 Class 1 (penetration resistance) or Class 2 (spall/shock resistance) specifications.
To defeat defined ballistic threat profiles under National Institute of Justice (NIJ) and NATO STANAG 4569 standards, defense systems rely on calibrated thicknesses of ballistic titanium plate. The engineering data below represents baseline single-plate requirements for monolithic Ti-6Al-4V at normal impact (0° obliquity).
| Threat Caliber & Projectile Type | Standard / Protection Level | Impact Velocity (m/s) | Minimum Plate Thickness (mm / in) | Areal Density (kg/m2) |
|---|---|---|---|---|
| 9×19mm FMJ Parabellum | NIJ Level II / HG1 | 398 ± 9 | 4.0 mm (0.157") | 17.8 kg/m2 |
| .44 Magnum SJHP | NIJ Level IIIA / HG2 | 436 ± 9 | 6.35 mm (0.250") | 28.2 kg/m2 |
| 5.56×45mm NATO (M193 Ball) | STANAG 4569 Level 1 | 940 ± 15 | 12.7 mm (0.500") | 56.4 kg/m2 |
| 7.62×39mm (Mild Steel Core / MSC) | NIJ Level III (Special Threat) | 720 ± 10 | 14.5 mm (0.570") | 64.3 kg/m2 |
| 7.62×51mm NATO (M80 Ball) | NIJ Level III / STANAG Level 1 | 847 ± 10 | 16.0 mm (0.630") | 71.0 kg/m2 |
| 7.62×51mm NATO AP (M61 Hard Core) | STANAG 4569 Level 2 | 830 ± 15 | 25.4 mm (1.000")* | 112.8 kg/m2 |
| 12.7×99mm (.50 BMG M2 Ball) | STANAG 4569 Level 3 (Partial) | 910 ± 15 | 38.1 mm (1.500") | 169.2 kg/m2 |
*Note: For hardened armor-piercing (AP) tungsten carbide cores, monolithic titanium is typically deployed as a structural backing plate combined with an ultra-hard ceramic face (e.g., Al2O3 or SiC) to shatter the penetrator tip before kinetic absorption.
Selecting the optimal ballistic material requires navigating structural tradeoffs among mass efficiency, multi-hit durability, fracture toughness, and environmental vulnerability.
| Performance Metric | Grade 5 Titanium (Ti-6Al-4V) | AR500 Ballistic Steel | Silicon Carbide Ceramic (SiC) |
|---|---|---|---|
| Density (g/cm3) | 4.43 g/cm3 (Weight-saving) | 7.85 g/cm3 (Heavy) | 3.15 g/cm3 (Ultra-light) |
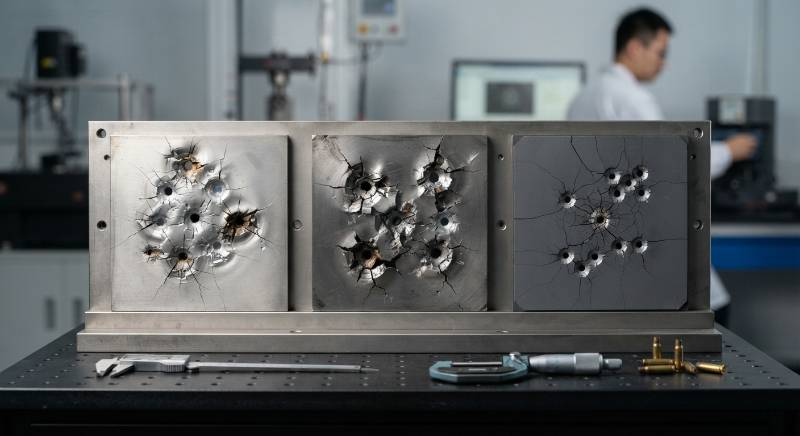
| Multi-Hit Durability | Exceptional (Plastic deformation) | High (High hardness) | Poor (Shatters on impact) |
| Spalling Hazard | Minimal (Captures fragments) | Severe (Requires anti-spall coat) | Severe (Requires composite wrap) |
| Corrosion Resistance | Immune (Saltwater/Marine) | Low (Prone to rust/oxidation) | High (Inert non-metal) |
| Structural Load Bearing | Yes (Dual structural/armor role) | Yes (Heavy structural vehicle hull) | No (Parasitic applique only) |
China Titanium Factory implements a rigorous thermomechanical manufacturing protocol engineered specifically to suppress adiabatic shear bands and maximize energy dissipation during impact.
Our metallurgical workflow integrates three core processing controls:
Vacuum Arc Double/Triple Remelting (VAR): Eliminates high-density inclusions and micro-segregation while holding interstitial oxygen below 0.16% for superior dynamic fracture toughness.
Thermomechanical Cross-Rolling: Replaces unidirectional rolling with multidirectional cross-rolling in the alpha-beta temperature regime. This creates an isotropic, non-directional grain structure that stops directional shear propagation.
Solution-Treated and Aged (STA) Conditioning: Calibrates the volumetric ratio of globular primary alpha phase within a transformed beta matrix, balancing yield strength (>880 MPa) and Charpy V-notch impact energy (>24 J at -40°C).
All finished armor components undergo full finishing via precision CNC titanium machining services and abrasive waterjet profiling to eliminate heat-affected zones (HAZ) along critical mounting edges.
Due to its combination of high strength, low density, and extreme corrosion resistance, ballistic titanium plate is standard equipment across mission-critical aerospace, defense, and maritime platforms:
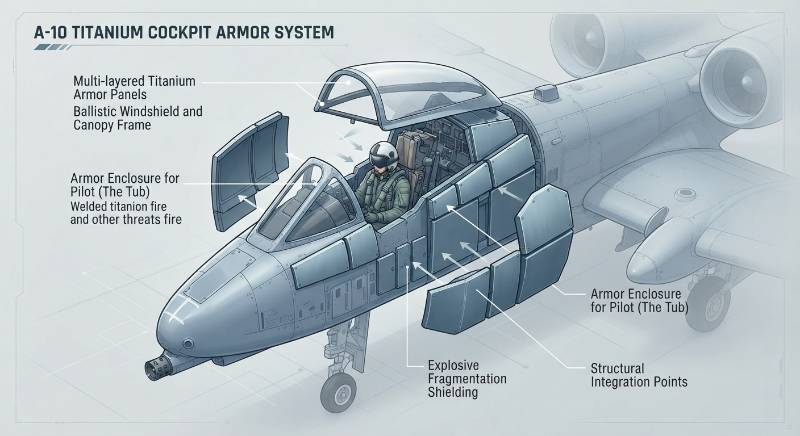
Aviation Cockpit Protection: The Fairchild Republic A-10 Thunderbolt II famously incorporates a monolithic Grade 5 titanium "bathtub" enclosure weighing over 540 kg, engineered to withstand direct 23mm anti-aircraft explosive cannon strikes.
Armored Combat Vehicles (AFVs): Replacing standard steel hatch covers, commanders' cupolas, and turret skirts with Ti-6Al-4V saves up to 40% in top-weight, lowering the vehicle's center of gravity and preserving powertrain service life.
Naval Blast & Anti-Splinter Bulkheads: Titanium provides complete immunity to marine chloride stress corrosion cracking while serving as combined structural bulkheads and secondary fragmentation barriers aboard modern surface combatants.
High-Mobility Tactical Ballistic Shields: Lightweight tactical entry shields manufactured from cross-rolled Ti-6Al-4V provide multi-hit rifle protection at a carry weight accessible to front-line breachers.
China Titanium Factory operates dedicated defense manufacturing lines capable of delivering certified titanium armor plates up to 100 mm in thickness, fully verified to global military and aerospace specifications.
Military Compliance: Certified to MIL-DTL-46077 Class 1 (High Penetration Resistance), Class 2 (High Toughness/Spall Resistance), and MIL-T-9046.
Aerospace Accreditations: AS9100D, ISO 9001:2015, and compliance with ASTM B265 and AMS 4911 standards.
Non-Destructive Testing (NDT): 100% AMS 2631 Class AA ultrasonic testing to guarantee void-free internal plate integrity.
MTC & Traceability: Complete EN 10204 3.1 Mill Test Certificates detailing full chemical melt history, interstitial gas levels, and Charpy impact data.
A standard 12.7×99mm (.50 BMG) ball round will penetrate monolithic Grade 5 titanium plates thinner than 38 mm (1.5 inches). When firing .50 BMG Armor-Piercing (AP M2) rounds with hardened tool steel or tungsten cores, solid titanium requires thicknesses exceeding 50 mm unless integrated into a composite array utilizing a ceramic strike face.
A 4.0 mm (0.157 inch) monolithic plate of Grade 5 (Ti-6Al-4V) is sufficient to stop standard 9×19mm FMJ handgun rounds fired at velocities up to 410 m/s, fully conforming to NIJ Level II / HG1 ballistic criteria.
Titanium produces far less spall and secondary fragmentation than ultra-hard AR500 steel plates. Due to its balanced modulus of elasticity (114 GPa) and superior ductility, titanium deforms plastically and captures bullet fragments within the strike indentation rather than deflecting lethal jacket shards radially toward the operator.
Authentic ballistic titanium must be verified through an EN 10204 3.1 Mill Test Certificate demonstrating an equiaxed alpha-beta microstructure, interstitial gas limits (O < 0.18%, H < 0.0125%), ultrasonic void inspection under AMS 2631, and minimum mechanical yield strength above 828 MPa.
China Titanium Factory provides a streamlined manufacturing pipeline for defense contractors, vehicle up-armorers, and aerospace engineering teams worldwide.
Step 1: Submit Drawing & Threat Caliber Specs: Send your CAD files, target STANAG/NIJ threat standards, and target dimensions directly to our engineering desk.
Step 2: 24-Hour DFM & Areal Mass Optimization: Our defense metallurgists return a comprehensive Design for Manufacturability (DFM) review, complete with plate weight calculations, tolerance schedules, and alloy recommendations.
Step 3: Rapid Prototyping & Certified Delivery: Receive mill-certified test plates manufactured to MIL-DTL-46077 and AS9100D standards, complete with full 3.1 traceability documentation and ultrasonic test reports.



Contact Us
Room 21003, 10th Floor, Unit 2, Building 1, Xianning International Plaza, No.29 Xianning West Road, Beilin District, Xi'an City
Copyright © Xi'an Shiguang Jingyan Technology Co., Ltd. All Rights Reserved.